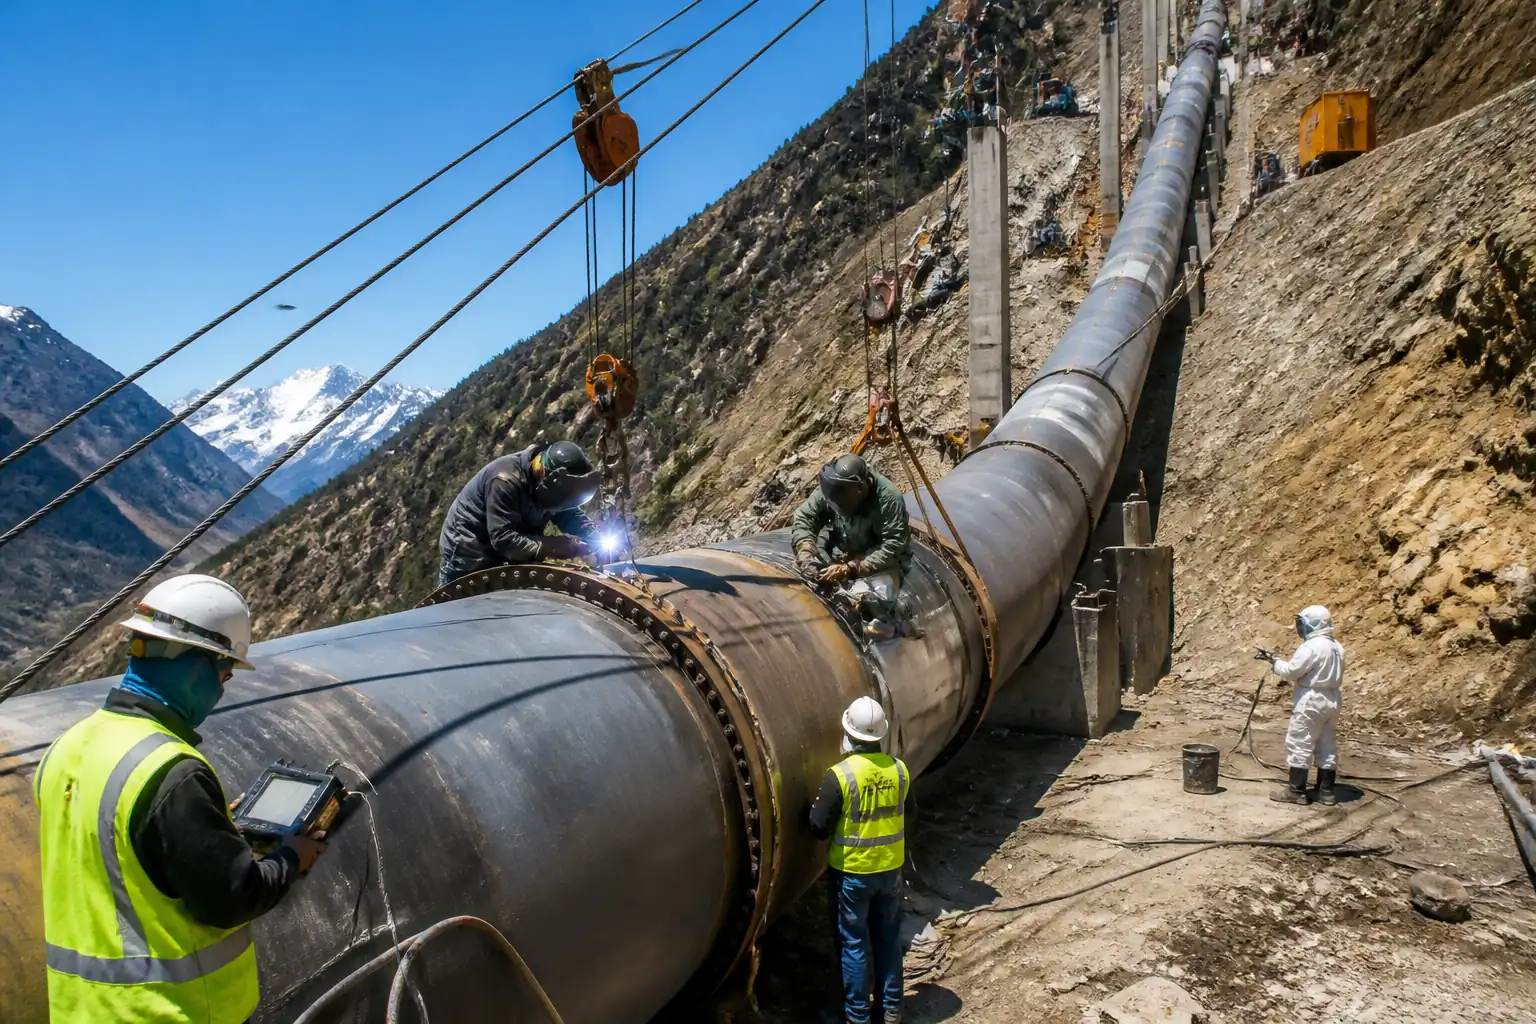
Inspection and Test Plan for Method Statement: Penstock Pipe Installation, Welding, Coating, and Hydrostatic Testing
AI-assisted inspection and test plan connected to a method statement, with PDF and Excel export.
More than a static template
Unlike a downloadable Word or PDF template, this ITP is an AI-assisted editable starting point directly connected to its method statement. Every inspection activity, hold point, and acceptance criterion is structured and ready to adapt to your project.
- AI-assisted customization — Tailor inspection activities and acceptance criteria to your specific project scope.
- Linked method statement — This ITP is connected to the corresponding method statement describing the work sequence.
- Multiple export formats — Download as a formatted PDF or editable Excel spreadsheet.
- Editable starting point, not a final document — Review and verify all content against your project specifications and standards before use.
What you can customize
When you save this ITP to your account, every inspection row becomes editable. You can add, remove, or modify:
- Inspection activity — Description of what is being inspected.
- Inspection type — Hold point (H), Witness point (W), Review (R), or Monitor (M).
- Responsibility — Contractor, subcontractor, engineer, or client.
- Frequency — How often the inspection occurs.
- Acceptance criteria — Referenced standard or specification requirement.
- Records — Forms, test reports, or checklists required as evidence.
Why this ITP is used
To verify that each construction step meets code, specification, and quality requirements before proceeding.
Who uses this inspection and test plan
QA/QC inspectors, site engineers, welding/coating inspectors, NDT personnel, and the Client’s representative.
When this ITP is prepared and submitted
Throughout construction from survey/set-out to final hydrostatic testing and handover.
Who receives or approves this ITP
Client/Engineer for review and approval.
Inspection scope
Dimensional controls, welding qualification and execution, 100% volumetric NDT, coating QA, and hydrotest verification.
Typical hold, witness, and review points
Fit-up (H), preheat (W), final VT (H), 100% UT/RT (H), surface prep (H), holiday test (H), hydrostatic test strength (H, Client), leak test (W).
Typical inspection records
Survey reports, fit-up and temperature logs, WPS/WQTR, NDT reports, coating QC records, holiday test, hydrotest certificates, calibration certs.
Important approval note
This ITP is an AI-assisted editable starting point, not a pre-approved document. Before use on any project, all inspection activities, hold points, and acceptance criteria must be reviewed and approved by the relevant parties (superintendent, principal contractor, or client representative) in accordance with your contract and project quality plan.
Always verify acceptance criteria against your applicable drawings, specifications, and regulatory requirements. Hold points must be confirmed with the relevant authority before work proceeds past that point.
Inspection and test plan
| Activity | Inspection / Test | Acceptance Criteria | Responsibility | Record |
|---|---|---|---|---|
| Survey and setting out | Verify control points, alignment and elevation checks | Within specified tolerances (±5 mm over 10 m) [Verify] | Surveyor / QC / Client | Survey report, ITP checklist |
| Incoming material verification | MTR review, dimensional/visual inspection | Compliant with material spec and drawings | QA/QC | Receiving inspection, MTR log |
| Rigging and temporary works pre-use | Certificates, visual checks, anchor verification | Per Temporary Works Design; valid certifications | Rigging Supervisor / QA/QC | Rigging checklists, certificates |
| Fit-up inspection | Root gap, hi–lo, bevel condition | Root gap 2–4 mm; hi–lo ≤10% t, max 3 mm; bevel sound | QC Inspector / Site Engineer | Fit-up report (photos) |
| Preheat/interpass control | Pyrometer/thermocouple readings | Per WPS; preheat typically 75–150°C; interpass ≤250°C [Verify] | Welder / QC | Temperature logs |
| Root pass VT and MT/PT (as specified) | Visual and MT/PT on root/tacks | No unacceptable indications; ISO 23277 Level 2 | QC / NDT Tech | VT/MT reports |
| Welding in progress | Parameter monitoring; interpass checks | Within WPS ranges; bead quality acceptable | Welding Engineer / QC | Welding logs |
| Final visual inspection of weld | VT using weld gauges | ISO 5817 Level B visual limits [Verify] | QC | VT report |
| Volumetric NDT (100% UT/PAUT or RT) | UT/PAUT or RT as per approved technique | ISO 11666 Level 2 (or project); zero unacceptable planar defects | NDT Level II/III | NDT report, weld map |
| Weld repair and re-examination (if any) | Repeat NDT over repaired area | Meets acceptance on re-test | Welding Engineer / NDT | RPR and NDT reports |
| Surface preparation inspection | Cleanliness (Sa 2½), profile, salt tests | ISO 8501-1 Sa 2½; profile 50–100 µm; salts ≤20 mg/m² | Coating Inspector | Surface prep report |
| Coating application inspection | DFT/WFT, environmental conditions | DFT within system TDS (e.g., 300–600 µm total) [Verify] | Coating Inspector | Coating QC report |
| Holiday detection | Holiday detector (voltage per NACE SP0188) | No holidays; all repaired and retested | Coating Inspector | Holiday test report |
| Hydrostatic test – strength | Pressurize to 1.25 × design; hold ≥2 h; monitor T/P | No leaks/distress; pressure stable within tolerance after temp correction | Hydrotest Engineer / QA/QC / Client | Strength test certificate, log sheets |
| Hydrostatic test – leak | Leak hold 8–24 h at specified pressure | No visible leakage; corrected pressure loss within instrument tolerance | Hydrotest Engineer / QA/QC | Leak test report |
| Draining, drying, reinstatement | Water quality checks if required; dew point (drying) | Discharge within permit; dryness per spec | CM / Environmental Officer | Draining log, environmental records |
This table is a read-only public reference. Download the PDF or Excel version, or customize this ITP to edit it for your project.
Frequently asked questions
Related method statement
This Inspection and Test Plan is associated with the Method Statement: Penstock Pipe Installation, Welding, Coating, and Hydrostatic Testing method statement, which describes the step-by-step construction sequence, resources, materials, equipment, safety controls, and environmental controls for this activity.
View the Method Statement: Penstock Pipe Installation, Welding, Coating, and Hydrostatic Testing method statement →