G
Guest

construction · 32 checks

3D Printed Concrete Inspection Checklist — Before, During & After Printing

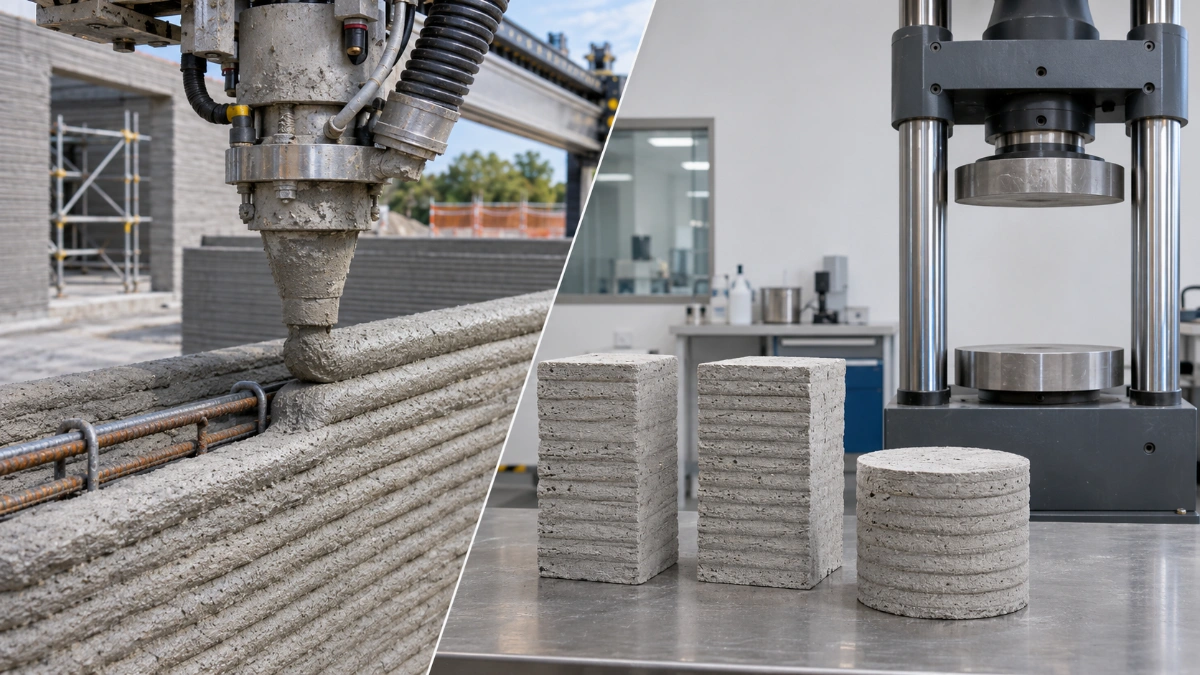
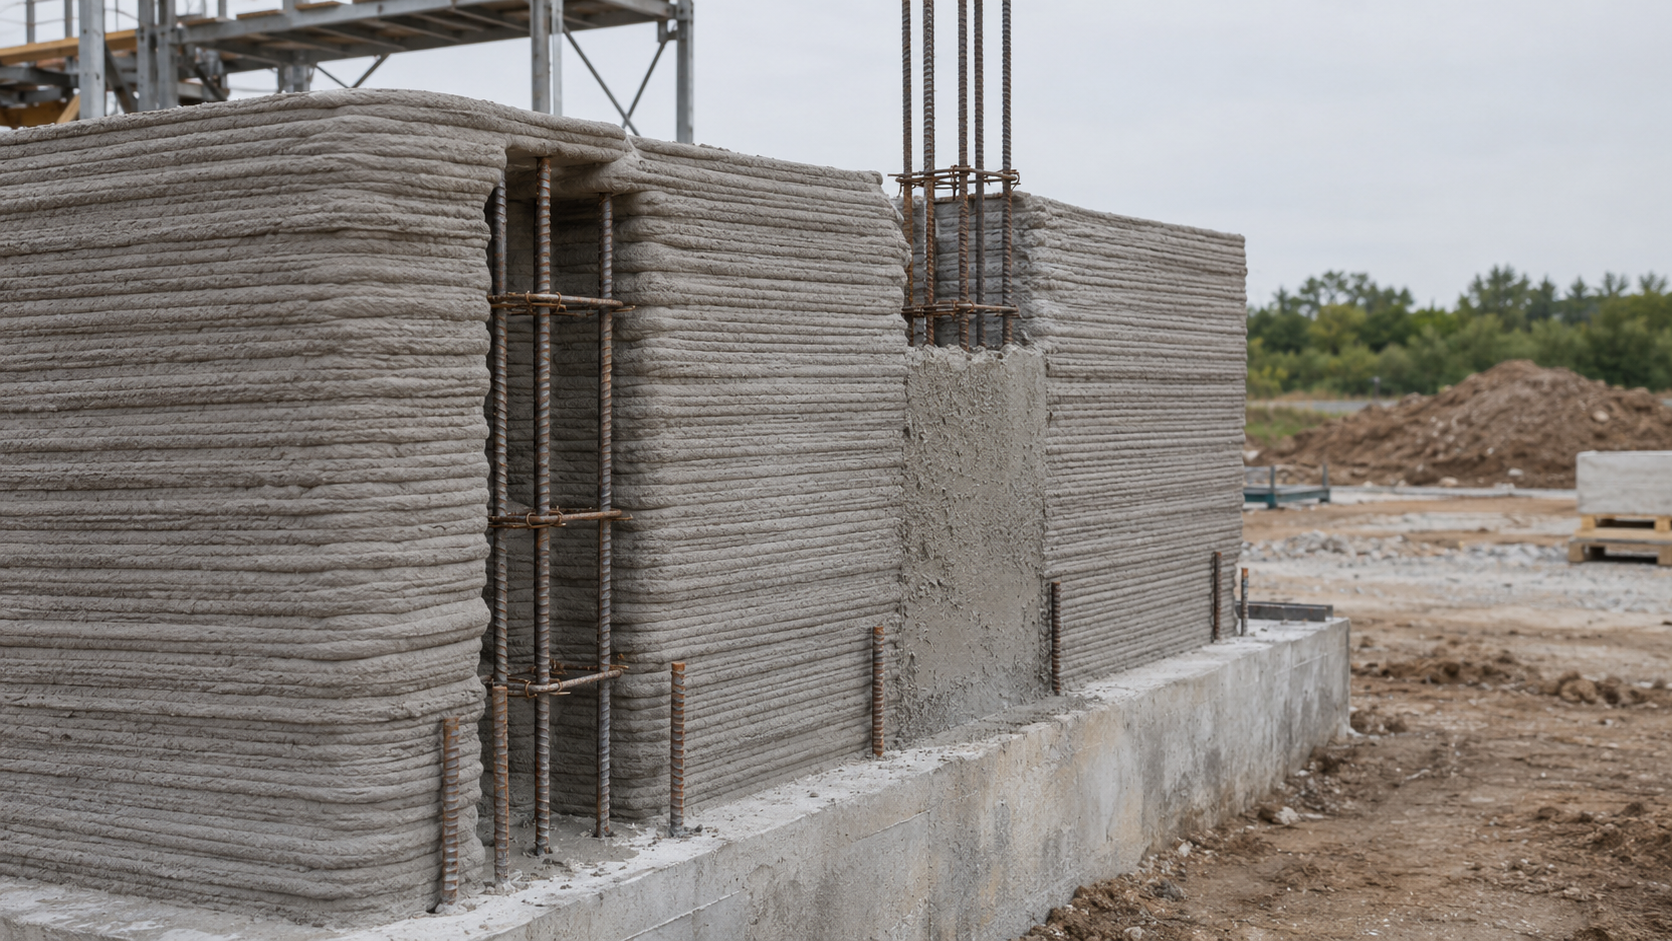
3D Printed Concrete Inspection Checklist — Before, During & After Printing is a practical, field-ready QA/QC tool for extrusion-based 3D concrete printing. It helps site engineers, inspectors, and contractors verify model/file control, material traceability, printer configuration, live process parameters, and final wall geometry. Unlike conventional concrete inspection, additive construction demands evidence of process history: which print file/toolpath revision ran, which batch was used, layer timing, interruptions, and how defects were handled. This checklist focuses on extrusion continuity, bead and layer geometry, alignment, buildability, and curing, while documenting reinforcement and embeds before concealment. Acceptance references the approved project specification, qualified printing system, method/procedure, ITP, manufacturer/system requirements, applicable codes/standards, and structural design—never universal limits. Use it to keep work within Hold/Witness/Surveillance points, log deviations, and support WIRs and NCRs where defined requirements are breached. Start in interactive mode to tick items, add comments, attach photos, and export PDF/Excel with a QR-secured record.

Create a construction QA/QC checklist titled:
3D Printed Concrete Inspection Checklist — Before, During & After Printing
Purpose
Create a practical field inspection checklist for site engineers, QA/QC engineers, inspectors and 3D-concrete-printing contractors inspecting extrusion-based 3D printed concrete walls.
The checklist must be usable during an actual print and should generate a professional supporting article explaining how to use it.
Important technical principle
3D printed concrete inspection must control both:
1. the finished wall, and
2. the printing process that produced it.
The checklist should therefore preserve evidence of:
- what was printed;
- which approved digital/model/print-file revision was used;
- which material batch was used;
- how the printer was configured;
- what happened during printing;
- interruptions and restart conditions;
- reinforcement and embeds;
- final geometry;
- defects;
- curing;
- specimens/testing; and
- final disposition/release.
Do not invent universal tolerances
Do not state generic millimetre limits, bead-offset percentages, maximum layer intervals or other numerical acceptance limits unless they are clearly identified as project/system-specific examples.
Acceptance must normally refer to:
- approved project specification;
- approved drawings/model;
- qualified printing system;
- approved method/procedure;
- Inspection and Test Plan (ITP);
- manufacturer/system requirements;
- structural design requirements; and
- applicable codes/standards.
Where a value is project-specific, provide a field such as:
Acceptance / Reference: __________
or
Specified value: ________
Terminology
Use Print File / Toolpath Revision, not only “G-code,” because not every printer exposes G-code.
Use:
- Hold
- Witness
- Surveillance
where appropriate.
Every inspection item should allow:
- Pass
- Fail
- N/A
- Recorded value / observation
- Evidence / photo reference
- Action / NCR / observation reference where relevant
Checklist structure
Header / traceability
Capture:
- Project
- Location
- Wall / Print Segment ID
- Grid / Element reference
- Inspection date and time
- WIR / Inspection reference
- Approved drawing/model revision
- Print file/toolpath revision
- Printer ID
- Nozzle/configuration ID if applicable
- Approved mix/material ID
- Batch/lot ID
- Operator
- Contractor representative
- QA/QC inspector
PHASE 1 — BEFORE PRINTING / PRE-PRINT RELEASE
Include inspection items for:
Document and digital control
- Approved drawing/model revision
- Approved print file/toolpath revision
- Wall geometry, cavities and openings
- Required reinforcement and embeds
- Approved method statement/procedure
- Applicable ITP inspection point
Survey and substrate
- Wall centreline / coordinates
- Corners and openings
- Foundation/substrate level
- Starting surface condition
- Starter bars/dowels/anchors
Printer setup and calibration
- Printer zero/reference point
- Coordinate-system alignment
- Printer level/setup
- Working envelope
- Motion path
- Collision clearance
- Calibration/verification status
Material traceability and readiness
- Approved mix/material ID
- Batch/lot
- Mixing/batching time
- Accelerator/admixture dosage where relevant
- Material within approved printing/open-time window
- Printability requirements satisfied
Do not imply that conventional slump alone establishes printability.
Reinforcement, embeds and MEP
- Vertical reinforcement
- Horizontal reinforcement/ties where relevant
- Anchors
- Sleeves
- Service ducts
- Electrical boxes
- Inserts
- Openings
- Items that will become inaccessible during printing
Environmental conditions
Record:
- Ambient temperature
- Relative humidity
- Wind
- Direct solar exposure
- Rain/weather risk
- Required protection against drying/skinning
Pre-print release
Include a clear:
READY TO PRINT / HOLD
decision.
PHASE 2 — DURING PRINTING / LIVE PROCESS CONTROL
Include:
Extrusion continuity
Inspect for:
- continuous flow;
- under-extrusion;
- over-extrusion;
- tearing;
- gaps;
- pump pulsation;
- nozzle blockage.
Bead and layer geometry
Record where required:
- bead width;
- layer height;
- wall thickness;
- cavity/shell dimensions.
Compare against the approved system requirements rather than inventing universal limits.
Layer alignment
Monitor:
- lateral offset;
- face alignment;
- corners/curves;
- cumulative dimensional drift.
Buildability
Inspect lower layers for:
- spreading;
- slumping;
- bulging;
- leaning;
- buckling;
- progressive deformation;
- local instability/collapse.
Nozzle clearance and contact
Check for:
- nozzle drag;
- collision;
- scraping of earlier layers;
- disturbance of reinforcement/embeds;
- changes in nozzle-to-wall clearance.
Note that nozzle contact can disturb still-fresh underlying layers and may affect interlayer contact beyond the visibly damaged surface.
Layer interval / timing
Record:
- relevant layer interval;
- planned pauses;
- unplanned pauses;
- comparison with approved maximum interval/restart procedure.
Do not use a universal “cold joint” limit.
Reinforcement and embeds installed during printing
Verify before concealment:
- horizontal ties;
- reinforcement;
- mesh;
- anchors;
- sleeves;
- service inserts;
- insulation if applicable.
Live defect monitoring
Include recognition of:
- tearing;
- under/over-extrusion;
- gaps;
- misalignment;
- slumping/bulging;
- nozzle damage;
- voids;
- poor layer contact;
- cracking;
- dimensional drift.
PRINT INTERRUPTION / RESTART RECORD
Make this a prominent dedicated subsection.
Record:
- wall/segment;
- layer/elevation;
- stop time;
- restart time;
- total downtime;
- reason;
- material batch before stop;
- material batch after restart;
- environmental conditions;
- exposed-layer condition;
- cleaning or surface preparation;
- additional material/treatment used;
- inspection before restart;
- approval/disposition;
- approved by.
MANDATORY STOP / HOLD CONDITIONS
Create a clearly visible warning section.
Examples of conditions requiring stop, hold or immediate technical review should include:
- physical wall location does not match digital/model coordinates;
- wrong print revision;
- missing structural reinforcement, anchor or critical embed;
- progressive bulging/buckling/instability;
- partial collapse;
- major extrusion discontinuity;
- significant nozzle collision;
- wall geometry progressively moving outside the approved envelope;
- interruption exceeding the approved restart/process limit;
- visible layer separation/delamination;
- any condition where continuing would conceal or worsen a nonconformance.
Distinguish between:
Immediate stop
and
Hold for engineering / QA disposition
where appropriate.
PHASE 3 — AFTER PRINTING / FINAL INSPECTION
As-built geometry
Check:
- wall location;
- wall length;
- total height;
- wall thickness;
- plumbness;
- straightness/alignment;
- openings;
- corners;
- connection zones;
- cavity dimensions where applicable.
Record survey/as-built reference.
Visual defects
Inspect for:
- tearing;
- gaps/voids;
- layer separation;
- restart interfaces;
- cracks;
- local deformation;
- exposed reinforcement;
- damaged surfaces;
- dimensional abnormalities.
Reinforcement / embeds / openings
Verify final position and presence of accessible:
- reinforcement;
- anchors;
- sleeves;
- penetrations;
- inserts;
- openings.
Curing and protection
Verify:
- approved curing method;
- start time;
- protection from drying;
- thermal/weather protection;
- protection from physical damage.
Test specimens and companion printed elements
Record:
- specimen IDs;
- companion wall/panel IDs;
- material batch link;
- scheduled test age(s);
- required test reference.
Do not hard-code 7- and 28-day testing as universal.
Cavity grouting / structural infill
Include only if applicable:
- cavity cleanliness;
- reinforcement;
- seals/formwork;
- readiness for grout/infill;
- release status.
Final release
Include:
- Accepted
- Accepted with comments / conditional
- Hold
- Rejected / NCR
and signatures/approval fields as appropriate.
DEFECT / DEVIATION LOG
Include a small structured register with:
- Location / layer / elevation
- Defect or deviation
- Photo/evidence reference
- Observation / NCR reference
- Engineering disposition
- Repair action
- Reinspection status
- Closure reference
Supporting article
Generate a supporting article explaining:
3D Printed Concrete Inspection Checklist: Before, During & After Printing
The article should:
- explain why inspection of 3D printed concrete differs from conventional concrete;
- explain that process history is part of the quality evidence;
- explain Hold / Witness / Surveillance points;
- explain the before/during/after workflow;
- explain why print interruptions need a dedicated record;
- explain that visible defects are not automatically structural failures;
- explain when printing should be stopped;
- explain that project/system-specific tolerances govern acceptance;
- explain that the normal project WIR can be used for inspection of printed work;
- mention that an NCR should be raised when a defined requirement has actually been breached;
- clearly state that the checklist is a practical project template and not a substitute for the approved ITP, structural design, qualified printing system or project specification.
Reference framework
Use current authoritative sources where applicable, particularly:
- ICC 1150-2026 — Standard for Automated Construction Technology for 3D Printing Walls
- ISO/ASTM 52939:2023 — Additive manufacturing for construction — Qualification principles
- relevant NIST additive construction / cement-based additive manufacturing research
Do not invent requirements that these sources do not contain.
Output / usability
The checklist should work well as:
- an interactive QChecklist;
- a printable PDF;
- an editable/exportable Excel record.
Keep field text concise enough for actual site use. Avoid long explanatory paragraphs inside checklist rows. Put explanations in the supporting article instead.
The final checklist should feel like a real QA/QC inspection record, not a blog summary.

3D Printed Concrete Inspection Checklist — Before, During & After Printing guides field QA/QC for extrusion-printed walls, capturing process, materials, geometry, defects, specimens, curing, and final release per approved requirements.

  • Controls finished wall and live printing process, not just outcomes
  • Preserves digital file, batch, setup, interruption and defect evidence
  • Aligns with approved ITP, drawings, procedures and qualified systems
  • Interactive, commentable, export, QR code for secure field records

The checklist

Header / Traceability

  1. Record Project, Location, Wall/Print Segment ID, Grid/Element reference, Inspection date/time, and WIR/Inspection reference. Tools: project forms/tablet. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Attach/record Approved drawing/model revision and Print File/Toolpath Revision (ID/checksum/link). Verify they match the intended wall segment. Tools: DMS, viewer. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  3. Record Printer ID, Nozzle/configuration ID, firmware/software version, calibration/verification status; Approved mix/material ID and Batch/Lot; Operator, Contractor representative, QA/QC inspector signatures. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Before Printing / Pre-Print Release: Document and Digital Control

  1. Confirm Approved drawings/model revision governs wall geometry, cavities, and openings; note any inconsistencies. Tools: model/drawing review. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Verify Approved method/procedure and applicable ITP points; confirm Hold/Witness/Surveillance stages for pre-print, live process, and final checks; confirm required reinforcement/embeds are defined. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Survey and Substrate

  1. Set out wall centreline, corners, and openings to coordinates. Record offsets to model. Tools: total station, targets. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Check foundation/substrate level and starting surface condition (clean, keyed/roughened as specified, dampness as required). Tools: level, moisture check, photos. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  3. Verify starter bars/dowels/anchors: type, location, projection, cleanliness, protection if specified. Tools: tape/gauge/photos. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Printer Setup and Calibration

  1. Establish printer zero/reference point to site datum; confirm coordinate-system alignment to grid; record transformation (e.g., offsets/rotation). Tools: survey tie-in, controller logs. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Verify level/setup, working envelope clearance, dry-run motion path, collision clearance, nozzle standoff, and calibration/verification status. Tools: electronic level, dry-run without material, standoff gauge. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Material Traceability and Readiness

  1. Confirm Approved mix/material ID vs tickets; record Batch/Lot, supplier, certificates; note admixtures by brand/lot. Tools: delivery tickets, register. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Record mixing/batching time and delivery to hopper; verify accelerator/admixture dosage setpoints and pump calibration; confirm material within approved open/printing-time window. Tools: batch logs, scales, pump settings. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  3. Perform printability checks per approved method (e.g., test bead, buildability/rheology indicators). Do not rely on slump alone. Tools: gauges, sample print. Mark Pass/Fail/NA. Record values, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Reinforcement, Embeds and MEP

  1. Verify vertical reinforcement size/spacing/position and clearance to print path; secure against movement. Tools: tape/cover gauge/photos. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Confirm horizontal ties/mesh to be inserted during printing are staged, identified by layer/elevation, and accessible. Tools: tags, insertion plan. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  3. Check anchors, sleeves, service ducts, electrical boxes, inserts, and openings: labeled, correct type/size/location; plan for items that become inaccessible. Tools: layout, photos. Mark Pass/Fail/NA. Record value/observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Environmental Conditions

  1. Record ambient temperature, relative humidity, wind, direct solar exposure, and rain/weather risk at start. Tools: meter, onsite log/photos. Mark Pass/Fail/NA. Record values, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Confirm protections against drying/skinning and weather (covers, windbreaks, curing materials) are available and deployed as required. Tools: visual check/photos. Mark Pass/Fail/NA. Record observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 1 — Pre-Print Release Decision

  1. READY TO PRINT / HOLD: Issue pre-print release or HOLD if any critical mismatch exists (files, survey, materials, reinforcement). Tools: WIR sign-off. Mark Pass/Fail/NA. Record decision, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 2 — During Printing: Extrusion Continuity

  1. Monitor continuous flow; identify under/over-extrusion, tearing, gaps, pump pulsation, or nozzle blockage; adjust per approved procedure. Tools: visual, flow logs. Mark Pass/Fail/NA. Record observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 2 — During Printing: Geometry, Alignment & Buildability

  1. At checkpoints measure bead width and layer height; record wall thickness and cavity/shell dimensions where accessible; compare to approved system/project requirements. Tools: calipers, gauges, probe/laser. Mark Pass/Fail/NA. Record values, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. Monitor lateral offset, face alignment, corners/curves, and cumulative drift; inspect lower layers for spreading, slumping, bulging, leaning, buckling, or instability. Tools: straightedge, level, visual. Mark Pass/Fail/NA. Record observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 2 — During Printing: Nozzle Clearance, Contact & Timing

  1. Check nozzle clearance; prevent drag/scraping or collisions with prior layers/embeds; verify layer interval timing including planned/unplanned pauses; compare to approved restart limits/procedures. Tools: standoff gauge, timer/logs. Mark Pass/Fail/NA. Record values, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 2 — During Printing: Reinforcement/Embeds & Live Defects

  1. Witness reinforcement, ties, mesh, anchors, sleeves, service inserts, insulation (if any) before concealment; photograph and log. Actively log defects (tearing, gaps, misalignment, slumping, voids, poor layer contact, cracking) and corrective actions. Mark Pass/Fail/NA. Record observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 2 — Print Interruption / Restart Record

  1. Record wall/segment, layer/elevation, stop time, restart time, total downtime, reason, material batch before/after, environmental conditions, exposed-layer condition, cleaning/surface prep, additional materials/treatment, inspection before restart, approval/disposition, and approved by. Mark Pass/Fail/NA. Record evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 2 — Mandatory Stop / Hold Conditions

  1. Immediate STOP if: wrong location or file revision; missing structural reinforcement/critical embed; progressive bulging/buckling/instability; partial collapse; major extrusion discontinuity; significant nozzle collision. Notify engineering/QA. Mark Pass/Fail/NA. Record observation, evidence/photo, action/NCR. Acceptance/Reference: __________
  2. HOLD for engineering/QA disposition if: geometry drifts outside approved envelope; interruption exceeds approved limit; visible layer separation/delamination; or continuing would conceal/worsen a nonconformance. Do not proceed without approval. Mark Pass/Fail/NA. Record observation, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 3 — After Printing / Final Inspection: As-Built & Visual

  1. Survey as-built wall location, length, height, thickness, plumbness, straightness/alignment, openings, corners, connection zones, cavities where applicable; map and photograph defects (tearing, voids, separations, restarts, cracks, deformation, exposed reinforcement). Tools: survey, gauges, photos. Mark Pass/Fail/NA. Record references, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 3 — After Printing / Final Inspection: Reinforcement & Openings

  1. Verify accessible reinforcement, anchors, sleeves, penetrations, inserts, and openings are present and within specified positions/clearances. Tools: tape/cover gauge/photos. Mark Pass/Fail/NA. Record values, evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 3 — After Printing / Final Inspection: Curing, Infill & Specimens

  1. Confirm approved curing method, start time, and protection (drying/thermal/physical). If cavity grouting/infill applies, verify cleanliness, reinforcement, seals/formwork, vents, and readiness. Record companion/specimen IDs, batch links, scheduled test ages, and test references. Mark Pass/Fail/NA. Record evidence/photo, action/NCR. Acceptance/Reference: __________

Phase 3 — Final Release

  1. Final disposition: Accepted / Accepted with comments (conditional) / HOLD / Rejected (NCR). Capture signatures/approvals and distribution. Tools: WIR closeout. Mark Pass/Fail/NA. Record decision rationale, evidence/photo, action/NCR. Acceptance/Reference: __________

Defect / Deviation Log

  1. Register entry: Location/layer/elevation; defect/deviation; photo/evidence ref; observation/NCR ref; engineering disposition; repair action; reinspection status; closure reference. Tools: log with QR-linked photos. Mark Pass/Fail/NA. Record details, evidence/photo, action/NCR. Acceptance/Reference: __________

Preview the printable checklist

Preview page one below. Open the image or download the PDF for all pages.
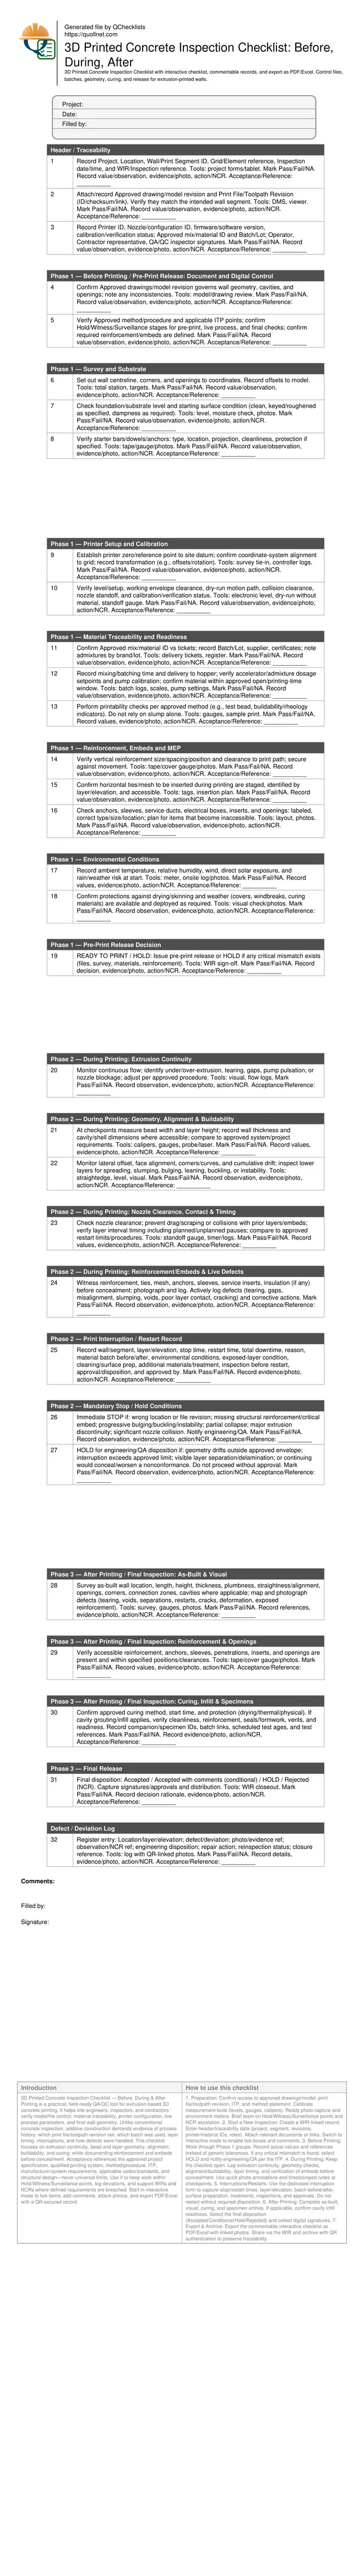
First-page preview of the 3D Printed Concrete Inspection printable checklist template.
3D Printed Concrete Inspection · Page 1 preview · Open image with all pages

At a glance

  • This checklist controls both finished wall compliance and the live extrusion process, recording approved model/file revisions, printer setup, material batches, layer timing, interruptions, and corrective actions to create defensible QA/QC evidence for additive concrete construction.
  • It aligns inspections with approved project specifications, drawings, qualified systems, manufacturer requirements, ITP points, and applicable standards, avoiding generic tolerances while capturing measured values, observations, photos, and references needed for WIRs and NCR decisions.
  • Interactive online checklist with tick, comment, and export features secured by QR code.
  • Usable during an active print, it prioritizes extrusion continuity, bead/layer geometry, alignment, buildability, nozzle clearance, and reinforcement/embeds before concealment—then verifies as-built geometry, curing, test specimens, and final release disposition.

How to Use This Checklist On Site

  1. Preparation: Confirm access to approved drawings/model, print file/toolpath revision, ITP, and method statement. Calibrate measurement tools (levels, gauges, calipers). Ready photo capture and environment meters. Brief team on Hold/Witness/Surveillance points and NCR escalation.
  2. Start a New Inspection: Create a WIR-linked record. Enter header/traceability data (project, segment, revisions, printer/material IDs, roles). Attach relevant documents or links. Switch to interactive mode to enable tick boxes and comments.
  3. Before Printing: Work through Phase 1 groups. Record actual values and references instead of generic tolerances. If any critical mismatch is found, select HOLD and notify engineering/QA per the ITP.
  4. During Printing: Keep the checklist open. Log extrusion continuity, geometry checks, alignment/buildability, layer timing, and verification of embeds before concealment. Use quick photo annotations and timestamped notes at checkpoints.
  5. Interruptions/Restarts: Use the dedicated interruption form to capture stop/restart times, layer/elevation, batch before/after, surface preparation, treatments, inspections, and approvals. Do not restart without required disposition.
  6. After Printing: Complete as-built, visual, curing, and specimen entries. If applicable, confirm cavity infill readiness. Select the final disposition (Accepted/Conditional/Hold/Rejected) and collect digital signatures.
  7. Export & Archive: Export the commentable interactive checklist as PDF/Excel with linked photos. Share via the WIR and archive with QR authentication to preserve traceability.

Choose a Focused 3D Concrete Printing Inspection

This 32-item master checklist covers the complete printing operation. For a specific site visit, use the focused checklist for that stage. For explanations of inspection responsibilities and acceptance records, see the 3D Printed Concrete Inspection Guide.

Why 3D-Printed Concrete Needs Process-Centric QA/QC

Inspection of 3D printed concrete differs from conventional concrete because the wall’s performance depends on both material properties and the layered extrusion process. Quality evidence must therefore include process history: which approved print file/toolpath revision ran, what batches were used, how the printer was configured, what timing and pauses occurred, and how defects were handled. Current frameworks such as ICC 1150-2026 and ISO/ASTM 52939:2023 emphasize qualified systems, documented procedures, traceable datasets, and defined inspection points. NIST research underscores the role of buildability and interlayer contact in structural outcomes. This checklist operationalizes those principles for field use, linking WIRs to drawings/models, approved procedures, and ITP Hold/Witness/Surveillance points. It avoids generic tolerances, instead steering inspectors to record measured values and reference the project specification, qualified system limits, manufacturer instructions, and structural design. The goal is repeatable, evidence-based accept/reject decisions without inventing universal millimetre limits.

  • Capture file/toolpath, batch, setup, timing, and defect history
  • Reference approved specs, drawings, ITP, and qualified system limits
  • Use Hold, Witness, and Surveillance to control key stages
  • Avoid universal tolerances; record values with references

Before–During–After Workflow That Works On Live Prints

The workflow starts before printing by confirming model/file control, survey and substrate readiness, printer calibration, and material printability. During printing, inspectors monitor extrusion continuity, bead and layer geometry, alignment, buildability, nozzle clearance, and layer timing—while verifying reinforcement and embeds before concealment. Every unplanned stop gets a dedicated interruption/restart record to document layer condition, cleaning, additional treatments, and approvals. After printing, as-built geometry and visual condition are surveyed, curing and protection are confirmed, companion specimens are logged, and final disposition is issued. Visible defects are not automatically structural failures; acceptance must align with the approved project specification, qualified system requirements, and design intent. Use the standard project WIR to anchor records, and raise an NCR only when a defined requirement is actually breached. This approach keeps production efficient while preserving the evidence needed for assurance and compliance.

  • Verify readiness and approvals before starting extrusion
  • Measure and log key dimensions at defined checkpoints
  • Record every interruption and restart with approvals
  • Base acceptance on project/system-specific criteria

Using Hold/Witness/Surveillance and Building a Defensible Record

Plan Hold points where work must pause for approval (e.g., pre-print release or restart after long pauses). Use Witness points to confirm transient steps such as embeds before concealment. Apply Surveillance during steady-state printing to spot drift, slumping, or nozzle contact. Each checklist line enables pass/fail/NA marking plus values, photos, and action references, supporting a clear audit trail tied to the WIR. Exports should include file/toolpath revision, batch IDs, environment, and survey references for traceability. When limits are project-specific, this checklist provides a blank “Acceptance/Reference” field so inspectors cite the correct clause or qualified system parameter. The result is a practical record compatible with ICC 1150-2026 and ISO/ASTM 52939:2023 expectations, while remaining efficient enough for active sites.

  • Use Hold for approvals; Witness for concealment points
  • Maintain continuous Surveillance during production
  • Cite the exact acceptance clause or system limit
  • Export a QR-secured, photo-rich WIR-backed record
Elie Saad's photo
Elie Saad
114198
539
33
49

Frequently asked questions

Why is 3D-printed concrete inspection different from conventional concrete?

Layered extrusion means wall performance depends on both mix behavior and the printing process. Inspectors must document file/toolpath revision, printer setup, batches, layer timing, interruptions, and live defects. Acceptance is then checked against the approved project specification, qualified system limits, and design intent—not generic tolerances.

When should we stop printing and place the work on HOLD?

Stop immediately for wrong location or file revision, missing critical reinforcement/embeds, instability or partial collapse, major extrusion discontinuity, or significant nozzle collision. Place on HOLD if geometry drifts outside the approved envelope, interruption exceeds the approved limit, delamination is visible, or continuing would conceal or worsen a nonconformance.

Do visible defects automatically mean structural failure?

No. Surface irregularities can exist without violating structural requirements. Evaluate defects against the approved specification, qualified system parameters, and design criteria. If a defined requirement is breached, raise an NCR; otherwise document, repair if directed, and seek engineering disposition where needed.

Which references govern acceptance for this checklist?

Use the approved project specification, drawings/model, qualified printing system documentation, approved method/procedure, ITP, manufacturer/system requirements, structural design, and applicable standards such as ICC 1150-2026 and ISO/ASTM 52939:2023, supplemented by relevant NIST research guidance where applicable.

Related Articles

Broader reading and guidance connected to this checklist topic.

3d Printed Concrete Inspection Checklist: Before, During & After Printing
3
en
3d Printed Concrete Inspection Checklist: Before, During & After Printing
EN
3d Printed Concrete Inspection Checklist: Before, During & After Printing

Field-ready 3D printed concrete inspection checklist covering pre-print release, live process checks, wall acceptance, defects, records and hold point...

Article 2026-11-06
3d Printed Concrete Qa/qc: Inspection, Process Control & Acceptance
3
en
3d Printed Concrete Qa/qc: Inspection, Process Control & Acceptance
EN
3d Printed Concrete Qa/qc: Inspection, Process Control & Acceptance

Practical QA/QC guide for 3D printed concrete walls: qualification, pre-print checks, live process control, interruptions, testing, defects and accept...

Article 2026-10-01
How Is 3d Printed Concrete Tested? Strength, Interlayer Bond & Acceptance
H
en
How Is 3d Printed Concrete Tested? Strength, Interlayer Bond & Acceptance
EN
How Is 3d Printed Concrete Tested? Strength, Interlayer Bond & Acceptance

How engineers test 3D printed concrete: printable mix qualification, representative specimens, compressive strength, interlayer bond, test orientation...

Article 2026-11-07
3d Printed Concrete Defects: Visual Field Guide For Site Engineers
3
en
3d Printed Concrete Defects: Visual Field Guide For Site Engineers
EN
3d Printed Concrete Defects: Visual Field Guide For Site Engineers

Visual field guide to 3D printed concrete defects: tearing, gaps, misalignment, slumping, restart interfaces, cracks, causes, records and escalation.

Article 2026-10-03
How Are 3d Printed Concrete Houses Reinforced? Rebar, Grouted Cores & Structural Connections
H
en
How Are 3d Printed Concrete Houses Reinforced? Rebar, Grouted Cores & Structural Connections
EN
How Are 3d Printed Concrete Houses Reinforced? Rebar, Grouted Cores & Structural Connections

How 3D printed concrete houses are reinforced: vertical bars, grouted cores, horizontal rebar, bond beams, foundation connections and QA/QC inspection...

Article 2026-11-08

Related Checklists

Keep the workflow moving with nearby templates chosen from similar checklist content.

QA inspectors check the layers of a 3D concrete wall as a robotic printer deposits fresh concrete. image
3
construction
3D Concrete Printing During-Print Quality Inspection Checklist
Construction
3D Concrete Printing During-Print Quality Inspection Checklist

Complete this checklist for one defined observation visit during active printing of a wall or segment. Repeat the checklist for later visits. Record l...

practical construction QA/QC checklist titled “Fresh Concrete Sampling Checklist” for site engineers, QA/QC inspectors and concrete technicians.

Keep the scope strictly limited to obtaining, handling and identifying a representative fresh-concrete sample before testing. Cover sampling location, timing, load/truck identification, delivery-ticket and mix reference, sampling method, composite or spot sampling where applicable, clean equipment, prevention of contamination or segregation, combining/remixing the sample where required, protecting the sample from environmental effects, prompt transfer for testing, and traceability to subsequent slump, temperature and cube/cylinder records.

Do not extend into:

performing the slump test;
measuring concrete temperature;
casting or curing cubes/cylinders;
deciding acceptance, rejection or retesting;
concrete placement or finishing;
detailed batch-ticket/mix compliance review;
admixture or water adjustment procedures.

Use project specifications and the applicable sampling standard as the governing requirements rather than inventing universal acceptance values. Make each checklist item practical, observable and suitable for recording evidence on site. image
F
construction
Fresh Concrete Sampling Checklist for QA/QC on Site
Construction
Fresh Concrete Sampling Checklist for QA/QC on Site

Fresh Concrete Sampling Checklist ensures field teams obtain, handle, and identify a representative fresh-concrete sample before testing. This practic...

Pile Cap Formwork/Rebar Inspection (Horizontal) Checklist image
P
construction
Pile Cap Formwork/Rebar Inspection (Horizontal) Checklist
Construction
Pile Cap Formwork/Rebar Inspection (Horizontal) Checklist

Pile Cap Formwork/Rebar Inspection (Horizontal) ensures a controlled, pre-pour verification of the pile cap’s formwork geometry and reinforcement. Thi...

Concrete slump test procedure using a slump cone (Abrams cone), tamping rod and measuring rule on a construction site image
C
construction
How to Perform a Concrete Slump Test: ASTM / EN Checklist
Construction
How to Perform a Concrete Slump Test: ASTM / EN Checklist

How to perform concrete slump test is the focus of this practical, field-ready checklist for site engineers and technicians. It walks you through slum...

Place pile cap concrete (horizontal) – Placement QA Checklist image
P
construction
Place pile cap concrete (horizontal) – Placement QA Checklist
Construction
Place pile cap concrete (horizontal) – Placement QA Checklist

Place pile cap concrete (horizontal) demands deliberate sequencing, controlled consolidation, precise finishing, and proactive curing. This checklist ...