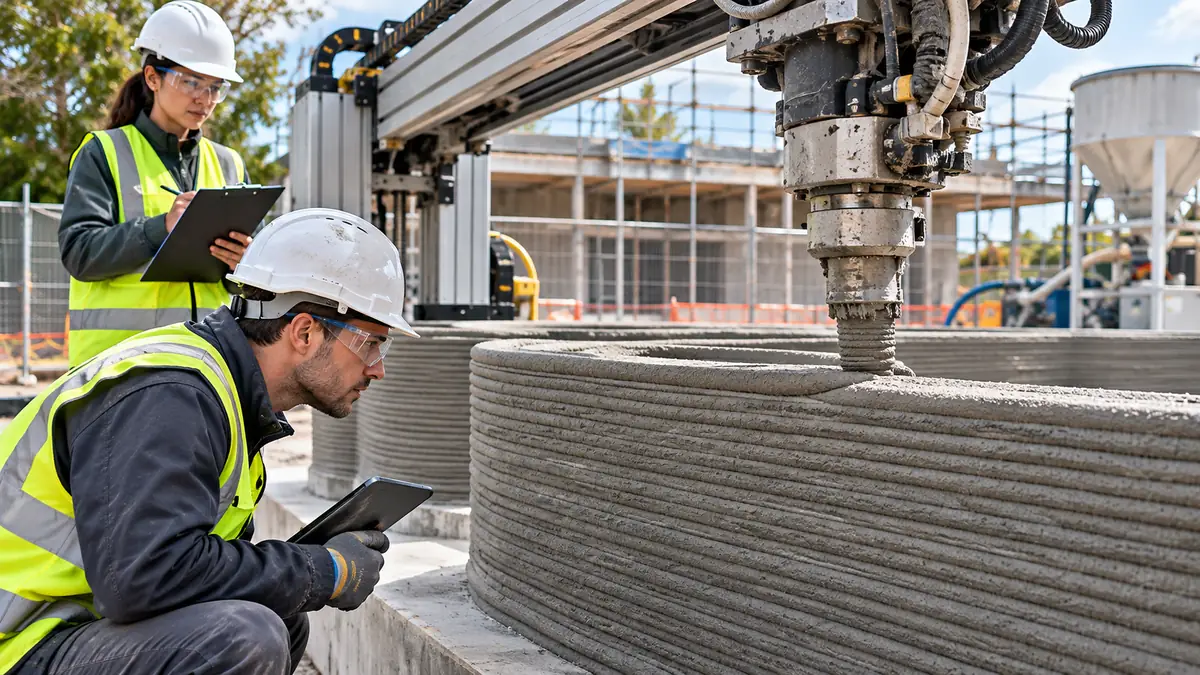
The checklist
Process identity
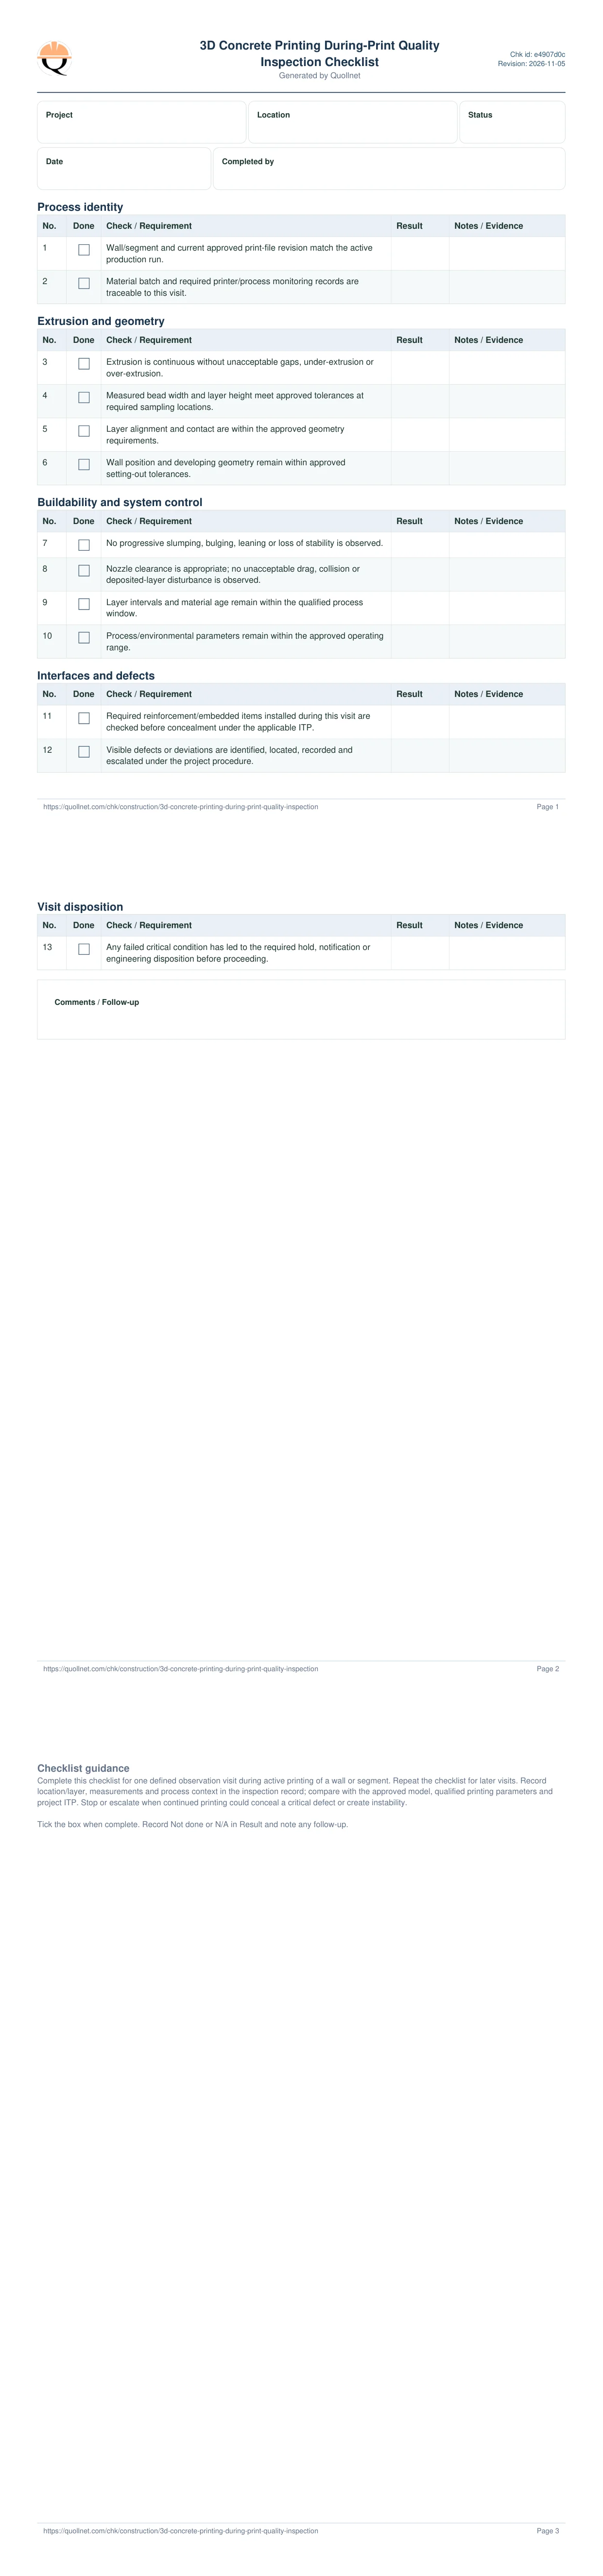
- Wall/segment and current approved print-file revision match the active production run.
- Material batch and required printer/process monitoring records are traceable to this visit.
Extrusion and geometry
- Extrusion is continuous without unacceptable gaps, under-extrusion or over-extrusion.
- Measured bead width and layer height meet approved tolerances at required sampling locations.
- Layer alignment and contact are within the approved geometry requirements.
- Wall position and developing geometry remain within approved setting-out tolerances.
Buildability and system control
- No progressive slumping, bulging, leaning or loss of stability is observed.
- Nozzle clearance is appropriate; no unacceptable drag, collision or deposited-layer disturbance is observed.
- Layer intervals and material age remain within the qualified process window.
- Process/environmental parameters remain within the approved operating range.
Interfaces and defects
- Required reinforcement/embedded items installed during this visit are checked before concealment under the applicable ITP.
- Visible defects or deviations are identified, located, recorded and escalated under the project procedure.
Visit disposition
- Any failed critical condition has led to the required hold, notification or engineering disposition before proceeding.
Preview the printable checklist
Preview page one below. Open the image or download the PDF for all pages.
At a glance
- For a single quality surveillance visit while a specific wall/segment is being printed.
- Observe extrusion, bead/layer geometry, layer contact, print stability, process timing and embedded items.
- No generic numeric limits: use the approved qualified process and project acceptance criteria.