Install wall joint waterstops field checklist guides site engineers and foremen on correct central placement, splicing, securing, and continuity inspection for wall construction joints only, excluding slab joints.
- Place centrally within wall thickness; verify equal embedment tolerances each side.
- Heat-weld splices with calibrated tools; confirm uniform bead and continuity.
- Secure to rebar and forms at set spacings; protect during pours.
- Interactive, commentable checklist with export and QR code verification.
The checklist
Pre-Pour Verification
- Confirm scope excludes slab joints; highlight wall joints only on drawings and ITP. Obtain supervisor sign-off and photo of marked drawings.
- Verify approved waterstop type, width, and profile per project specifications; record product data, lot numbers, and delivery dockets with photos.
- Inspect storage: waterstops straight, clean, shaded, 5–35°C; log temperature and capture storage condition photos.
- Review joint layout for continuous path across construction/expansion joints, corners, and penetrations; markup continuity on drawings and attach to checklist.
Materials & Tools
- Prepare calibrated thermostatic heat welder (per manufacturer range), splicing jigs, clamps, guillotine cutter; attach calibration certificate and tool photos.
- Provide stainless tying wire or hog rings, approved clips, and tie spacing template at 150–200 mm centres; photograph kit before use.
- Check stop-end/bulkhead forms with central slot sized to waterstop width ±2 mm; record measurement and photo of slot gauge.
Placement & Alignment
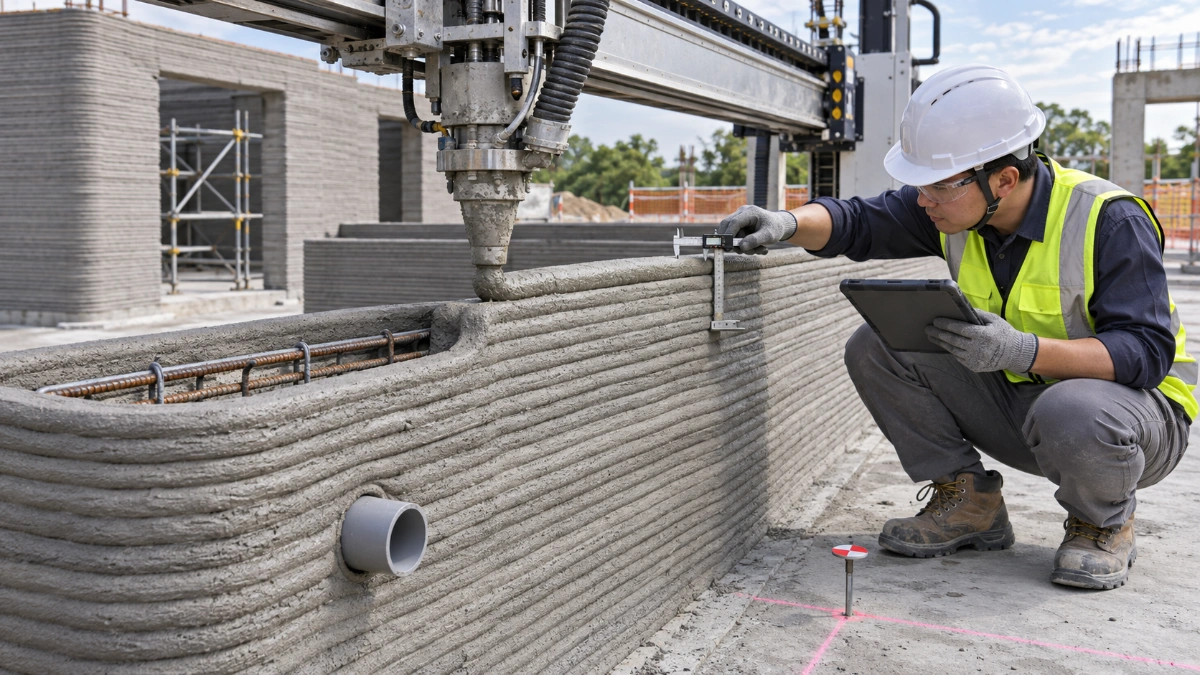
- Mark joint centerline on rebar or formwork; tolerance ±5 mm. Capture measurement photo with steel rule.
- Position the waterstop centrally in wall thickness; verify equal embedment each side within ±10 mm using gauge rod; record readings.
- Align bulb/dumbbell without twist; twist ≤5°. Photograph along length showing flat flanges and straight profile.
- Maintain minimum 50 mm concrete cover to reinforcement and ensure unobstructed concrete flow paths; document with photos.
- Anchor using factory eyelets or flange fastening only; do not puncture the bulb/web. Take close-up photo of fixings.
Splicing & Transitions
- Cut ends square with guillotine; clean and dry faces; bag off dust. Photograph prepared ends prior to welding.
- Heat-weld butt splices in jig; confirm continuous weld bead 3–5 mm wide with no voids; perform bend/peel check and take photos.
- Use pre-moulded tees/crosses/corners where required; if field-fabricated, assemble per manufacturer guidance and record approval with close-up photos.
- Locate splices ≥300 mm from corners or bulkheads; mark splice stations on drawings and tag on the element; attach map photo.
Securing & Concrete Operations
- Tie flanges to rebar at 150–200 mm centres; ties snug, no distortion. Provide sequence photos every 1.5 m.
- Fix to formwork with brass nails/clips through flanges only at 200 mm centres; nail heads flush; capture close-ups.
- Install protective cover over exposed half before first pour; remove before second pour; document installation and removal with timestamps.
- Maintain ≥50 mm clearance from internal vibrators to the bulb; brief crew and log toolbox talk with signatures.
- Seal bulkhead slot and interfaces to prevent grout loss using approved foam/mastic; inspect edges and take photos pre-pour.
Inspection & Records
- Verify continuity end-to-end with visual trace; no gaps or misalignment; produce photo map with stationing.
- After first lift set, confirm exposed half is clean, undamaged, and protected; photo evidence and QA sign-off required.
- Before closing second side, recheck alignment, ties, and all splices; record checklist status and engineer’s signature.
- Compile as-builts: splice locations, lot numbers, elevations, and photos; upload to document control with QR link.
- If damaged, repair with approved patch piece extending ≥150 mm each side; re-weld, re-inspect, and close NCR with photos.
Preview the printable checklist
Preview page one below. Open the image or download the PDF for all pages.
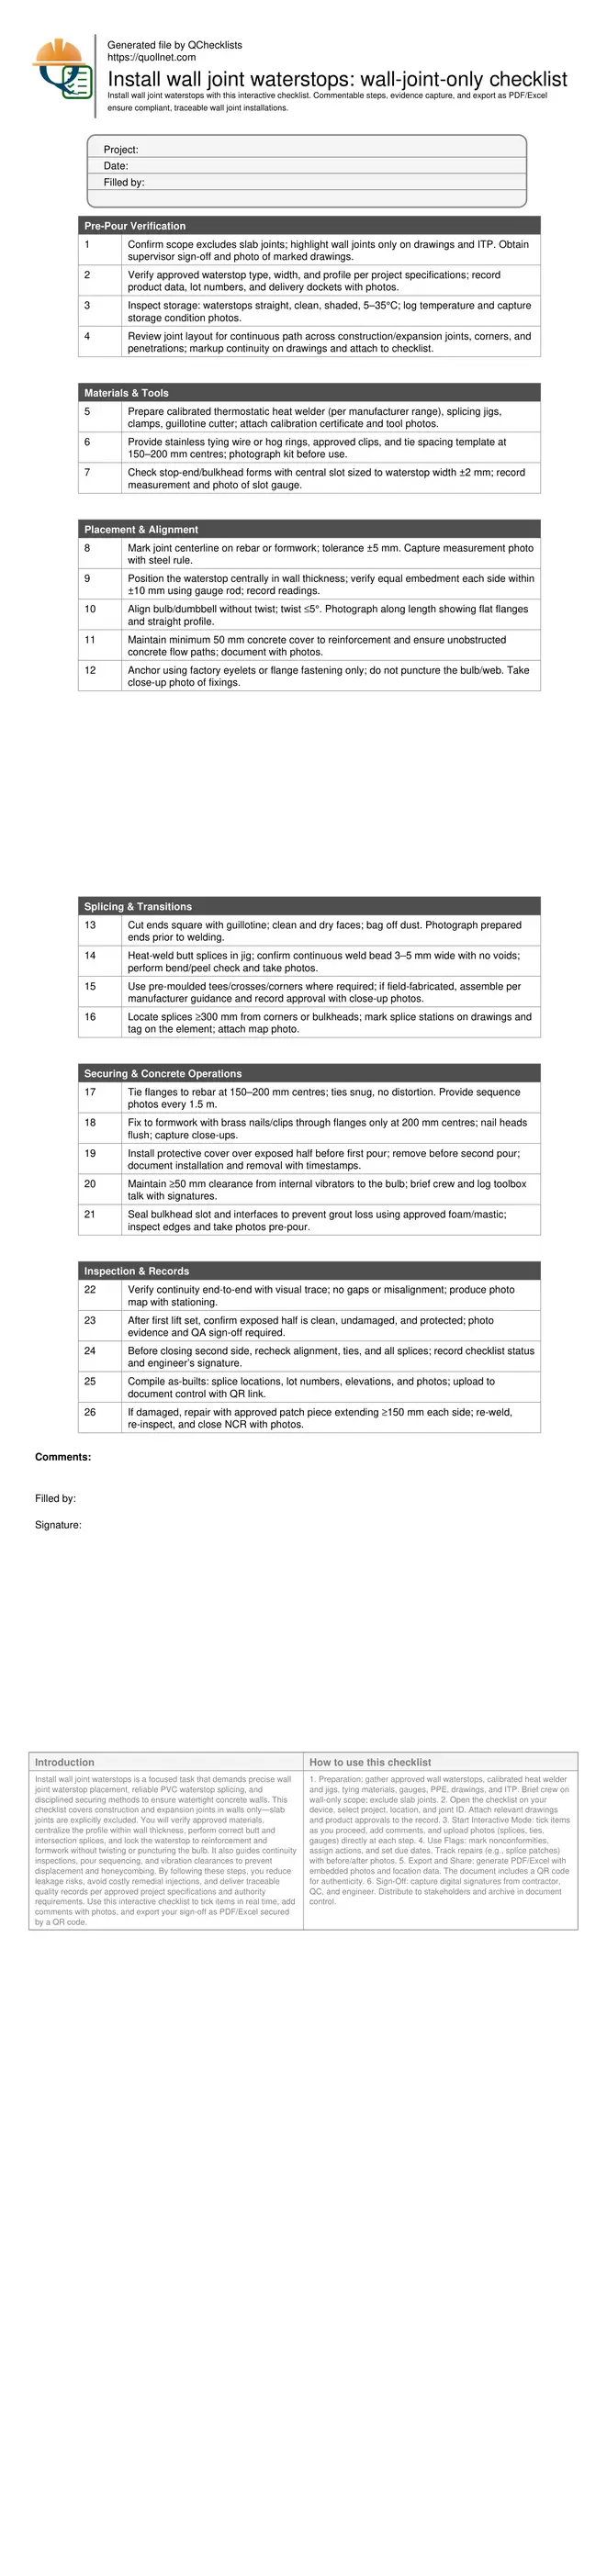
At a glance
- Centrally positioned waterstops with verified equal embedment and twist limits create reliable barriers against hydrostatic pressure, reducing leakage pathways at wall construction and expansion joints. The checklist standardizes alignment, tie spacing, and formwork interfaces to prevent displacement during concrete placement and vibration.
- Quality splicing is decisive for continuity. Field teams use calibrated heat-welding jigs, control temperature windows, and confirm uniform bead dimensions. Pre-moulded intersections or approved fabrications address tees and corners, while documented photos and marked drawings ensure traceable, auditable closure of all splice locations.
- Concrete operations can compromise performance if not controlled. The checklist enforces protective measures for exposed halves, minimum clearances from vibrators, and grout tightness at bulkheads. It also sequences inspections before closing forms, ensuring defects are corrected early and continuity is maintained end-to-end.
- Interactive online checklist with tick, comment, and export features secured by QR code.
How to Use This Interactive Checklist
- Preparation: gather approved wall waterstops, calibrated heat welder and jigs, tying materials, gauges, PPE, drawings, and ITP. Brief crew on wall-only scope; exclude slab joints.
- Open the checklist on your device, select project, location, and joint ID. Attach relevant drawings and product approvals to the record.
- Start Interactive Mode: tick items as you proceed, add comments, and upload photos (splices, ties, gauges) directly at each step.
- Use Flags: mark nonconformities, assign actions, and set due dates. Track repairs (e.g., splice patches) with before/after photos.
- Export and Share: generate PDF/Excel with embedded photos and location data. The document includes a QR code for authenticity.
- Sign-Off: capture digital signatures from contractor, QC, and engineer. Distribute to stakeholders and archive in document control.
Central Placement, Alignment, and Concrete Flow
Waterstops must sit on the wall’s centerline to provide equal embedment and reliable sealing. Start by marking the joint centerline and using a gauge rod to verify the profile is within ±10 mm of equal embedment each side. Keep the bulb and webs straight with twist limited to 5° so the ribs engage consistently. Maintain at least 50 mm clearance to reinforcement and allow open flow paths for concrete to pass through and around the profile. Congested cages benefit from pre-planned tie points, temporary spreaders, and staged tying from the centre outward to avoid pull or bow. Avoid puncturing the bulb; fix only through flanges using appropriate clips or brass nails. A practical cue is to sight along 2–3 m runs before pour and photograph alignment with a straightedge for record. These controls reduce displacement when internal vibrators operate and prevent honeycombing that compromises watertightness.
- Mark the centerline and verify equal embedment within ±10 mm.
- Limit twist to 5°; keep flanges flat and straight.
- Maintain 50 mm minimum clearance to reinforcement.
- Create open concrete flow paths around the profile.
- Fix through flanges only; never puncture the bulb.
Splicing Quality, Intersections, and Continuity Control
Continuity depends on clean, square cuts and calibrated heat-welding. Use a guillotine for square faces, keep surfaces dry, and weld in a manufacturer-approved jig. Control temperature and dwell to achieve a continuous 3–5 mm external bead with no voids. After cooling, perform bend/peel checks and photograph the bead. Use pre-moulded intersections for tees and corners where available; otherwise, field-fabricate per approved details and document approvals. Place splices at least 300 mm away from corners and bulkheads to reduce stress concentrations. Tag splice stations on the element and mark them on drawings for traceability. Before each pour, visually trace the entire path to confirm an unbroken line and secure flanges at 150–200 mm centres. This approach, combined with robust records, allows rapid verification by supervisors and authorities and minimizes rework costs from leaks.
- Cut ends square; clean and dry before welding.
- Use calibrated welder and approved splicing jig.
- Target a uniform 3–5 mm weld bead.
- Keep splices ≥300 mm from corners/bulkheads.
- Map and photograph every splice location.
Securing, Pour Sequencing, and Vibration Practices
Proper securing keeps the waterstop in place during both pours. Tie flanges to rebar at 150–200 mm centres and anchor to formwork through flanges with brass nails or clips. Install protective covers over the exposed half before the first pour to prevent paste contamination, then remove before closing and the second pour. At bulkheads, seal slots and edges to prevent grout loss. During placement, maintain at least 50 mm clearance from internal vibrators to the bulb; brief crews and nominate a spotter to watch for movement. After the first lift sets, inspect the exposed half for damage or contamination and resecure as needed. Before closing forms, recheck alignment, ties, and all splices. Record all findings with timestamped photos and update as-builts to capture lot numbers, splice stations, and elevations for future reference and compliance.
- Tie flanges at 150–200 mm centres to rebar.
- Protect exposed half before first pour.
- Seal bulkhead slots to prevent grout loss.
- Keep vibrators ≥50 mm from the bulb.
- Reinspect before closing and second pour.