G
Guest

Create a construction QA/QC checklist titled:
3D Printed Concrete Inspection Checklist — Before, During & After Printing
Purpose
Create a practical field inspection checklist for site engineers, QA/QC engineers, inspectors and 3D-concrete-printing contractors inspecting extrusion-based 3D printed concrete walls.
The checklist must be usable during an actual print and should generate a professional supporting article explaining how to use it.
Important technical principle
3D printed concrete inspection must control both:
1. the finished wall, and
2. the printing process that produced it.
The checklist should therefore preserve evidence of:
- what was printed;
- which approved digital/model/print-file revision was used;
- which material batch was used;
- how the printer was configured;
- what happened during printing;
- interruptions and restart conditions;
- reinforcement and embeds;
- final geometry;
- defects;
- curing;
- specimens/testing; and
- final disposition/release.
Do not invent universal tolerances
Do not state generic millimetre limits, bead-offset percentages, maximum layer intervals or other numerical acceptance limits unless they are clearly identified as project/system-specific examples.
Acceptance must normally refer to:
- approved project specification;
- approved drawings/model;
- qualified printing system;
- approved method/procedure;
- Inspection and Test Plan (ITP);
- manufacturer/system requirements;
- structural design requirements; and
- applicable codes/standards.
Where a value is project-specific, provide a field such as:
Acceptance / Reference: __________
or
Specified value: ________
Terminology
Use Print File / Toolpath Revision, not only “G-code,” because not every printer exposes G-code.
Use:
- Hold
- Witness
- Surveillance
where appropriate.
Every inspection item should allow:
- Pass
- Fail
- N/A
- Recorded value / observation
- Evidence / photo reference
- Action / NCR / observation reference where relevant
Checklist structure
Header / traceability
Capture:
- Project
- Location
- Wall / Print Segment ID
- Grid / Element reference
- Inspection date and time
- WIR / Inspection reference
- Approved drawing/model revision
- Print file/toolpath revision
- Printer ID
- Nozzle/configuration ID if applicable
- Approved mix/material ID
- Batch/lot ID
- Operator
- Contractor representative
- QA/QC inspector
PHASE 1 — BEFORE PRINTING / PRE-PRINT RELEASE
Include inspection items for:
Document and digital control
- Approved drawing/model revision
- Approved print file/toolpath revision
- Wall geometry, cavities and openings
- Required reinforcement and embeds
- Approved method statement/procedure
- Applicable ITP inspection point
Survey and substrate
- Wall centreline / coordinates
- Corners and openings
- Foundation/substrate level
- Starting surface condition
- Starter bars/dowels/anchors
Printer setup and calibration
- Printer zero/reference point
- Coordinate-system alignment
- Printer level/setup
- Working envelope
- Motion path
- Collision clearance
- Calibration/verification status
Material traceability and readiness
- Approved mix/material ID
- Batch/lot
- Mixing/batching time
- Accelerator/admixture dosage where relevant
- Material within approved printing/open-time window
- Printability requirements satisfied
Do not imply that conventional slump alone establishes printability.
Reinforcement, embeds and MEP
- Vertical reinforcement
- Horizontal reinforcement/ties where relevant
- Anchors
- Sleeves
- Service ducts
- Electrical boxes
- Inserts
- Openings
- Items that will become inaccessible during printing
Environmental conditions
Record:
- Ambient temperature
- Relative humidity
- Wind
- Direct solar exposure
- Rain/weather risk
- Required protection against drying/skinning
Pre-print release
Include a clear:
READY TO PRINT / HOLD
decision.
PHASE 2 — DURING PRINTING / LIVE PROCESS CONTROL
Include:
Extrusion continuity
Inspect for:
- continuous flow;
- under-extrusion;
- over-extrusion;
- tearing;
- gaps;
- pump pulsation;
- nozzle blockage.
Bead and layer geometry
Record where required:
- bead width;
- layer height;
- wall thickness;
- cavity/shell dimensions.
Compare against the approved system requirements rather than inventing universal limits.
Layer alignment
Monitor:
- lateral offset;
- face alignment;
- corners/curves;
- cumulative dimensional drift.
Buildability
Inspect lower layers for:
- spreading;
- slumping;
- bulging;
- leaning;
- buckling;
- progressive deformation;
- local instability/collapse.
Nozzle clearance and contact
Check for:
- nozzle drag;
- collision;
- scraping of earlier layers;
- disturbance of reinforcement/embeds;
- changes in nozzle-to-wall clearance.
Note that nozzle contact can disturb still-fresh underlying layers and may affect interlayer contact beyond the visibly damaged surface.
Layer interval / timing
Record:
- relevant layer interval;
- planned pauses;
- unplanned pauses;
- comparison with approved maximum interval/restart procedure.
Do not use a universal “cold joint” limit.
Reinforcement and embeds installed during printing
Verify before concealment:
- horizontal ties;
- reinforcement;
- mesh;
- anchors;
- sleeves;
- service inserts;
- insulation if applicable.
Live defect monitoring
Include recognition of:
- tearing;
- under/over-extrusion;
- gaps;
- misalignment;
- slumping/bulging;
- nozzle damage;
- voids;
- poor layer contact;
- cracking;
- dimensional drift.
PRINT INTERRUPTION / RESTART RECORD
Make this a prominent dedicated subsection.
Record:
- wall/segment;
- layer/elevation;
- stop time;
- restart time;
- total downtime;
- reason;
- material batch before stop;
- material batch after restart;
- environmental conditions;
- exposed-layer condition;
- cleaning or surface preparation;
- additional material/treatment used;
- inspection before restart;
- approval/disposition;
- approved by.
MANDATORY STOP / HOLD CONDITIONS
Create a clearly visible warning section.
Examples of conditions requiring stop, hold or immediate technical review should include:
- physical wall location does not match digital/model coordinates;
- wrong print revision;
- missing structural reinforcement, anchor or critical embed;
- progressive bulging/buckling/instability;
- partial collapse;
- major extrusion discontinuity;
- significant nozzle collision;
- wall geometry progressively moving outside the approved envelope;
- interruption exceeding the approved restart/process limit;
- visible layer separation/delamination;
- any condition where continuing would conceal or worsen a nonconformance.
Distinguish between:
Immediate stop
and
Hold for engineering / QA disposition
where appropriate.
PHASE 3 — AFTER PRINTING / FINAL INSPECTION
As-built geometry
Check:
- wall location;
- wall length;
- total height;
- wall thickness;
- plumbness;
- straightness/alignment;
- openings;
- corners;
- connection zones;
- cavity dimensions where applicable.
Record survey/as-built reference.
Visual defects
Inspect for:
- tearing;
- gaps/voids;
- layer separation;
- restart interfaces;
- cracks;
- local deformation;
- exposed reinforcement;
- damaged surfaces;
- dimensional abnormalities.
Reinforcement / embeds / openings
Verify final position and presence of accessible:
- reinforcement;
- anchors;
- sleeves;
- penetrations;
- inserts;
- openings.
Curing and protection
Verify:
- approved curing method;
- start time;
- protection from drying;
- thermal/weather protection;
- protection from physical damage.
Test specimens and companion printed elements
Record:
- specimen IDs;
- companion wall/panel IDs;
- material batch link;
- scheduled test age(s);
- required test reference.
Do not hard-code 7- and 28-day testing as universal.
Cavity grouting / structural infill
Include only if applicable:
- cavity cleanliness;
- reinforcement;
- seals/formwork;
- readiness for grout/infill;
- release status.
Final release
Include:
- Accepted
- Accepted with comments / conditional
- Hold
- Rejected / NCR
and signatures/approval fields as appropriate.
DEFECT / DEVIATION LOG
Include a small structured register with:
- Location / layer / elevation
- Defect or deviation
- Photo/evidence reference
- Observation / NCR reference
- Engineering disposition
- Repair action
- Reinspection status
- Closure reference
Supporting article
Generate a supporting article explaining:
3D Printed Concrete Inspection Checklist: Before, During & After Printing
The article should:
- explain why inspection of 3D printed concrete differs from conventional concrete;
- explain that process history is part of the quality evidence;
- explain Hold / Witness / Surveillance points;
- explain the before/during/after workflow;
- explain why print interruptions need a dedicated record;
- explain that visible defects are not automatically structural failures;
- explain when printing should be stopped;
- explain that project/system-specific tolerances govern acceptance;
- explain that the normal project WIR can be used for inspection of printed work;
- mention that an NCR should be raised when a defined requirement has actually been breached;
- clearly state that the checklist is a practical project template and not a substitute for the approved ITP, structural design, qualified printing system or project specification.
Reference framework
Use current authoritative sources where applicable, particularly:
- ICC 1150-2026 — Standard for Automated Construction Technology for 3D Printing Walls
- ISO/ASTM 52939:2023 — Additive manufacturing for construction — Qualification principles
- relevant NIST additive construction / cement-based additive manufacturing research
Do not invent requirements that these sources do not contain.
Output / usability
The checklist should work well as:
- an interactive QChecklist;
- a printable PDF;
- an editable/exportable Excel record.
Keep field text concise enough for actual site use. Avoid long explanatory paragraphs inside checklist rows. Put explanations in the supporting article instead.
The final checklist should feel like a real QA/QC inspection record, not a blog summary. image
3
3D Printed Concrete Inspection Checklist: Before, During, After
construction quality assurance +2

3D Printed Concrete Inspection Checklist with interactive checklist, commentable records, and export as PDF/Excel. Control files, batches, geometry, curing, and release for extrusion-printed walls.
A worker handling a round corrugated metal air duct on the floor of an unfinished concrete room, illuminated by temporary work lights and overhead piping. image
R
Rectangular Duct Transverse Joint Sealing Inspection (Pre-Insulation) Guide
construction quality assurance +1

Inspect rectangular duct transverse joint sealing before insulation: verify alignment, gaskets, and continuous exterior seals at seams, corners, and penetrations.
Inspector checks reinforcement and embedded conduits in a 3D printed concrete wall before concealment. image
3
3D Printed Concrete Reinforcement and Embedded Services Inspection Checklist
construction quality assurance +1

3D Printed Concrete Reinforcement and Embedded Services Inspection Checklist for one 3D concrete printing site visit, using approved project tolerances and documented inspection releases.
Inspect precast façade panel lifting anchors & rigging image
P
Inspect precast façade panel lifting anchors & rigging
construction safety +3

Inspect precast façade panel lifting anchors and rigging readiness using an interactive checklist that’s commentable and can export as PDF/Excel for traceable, on-site sign-off.
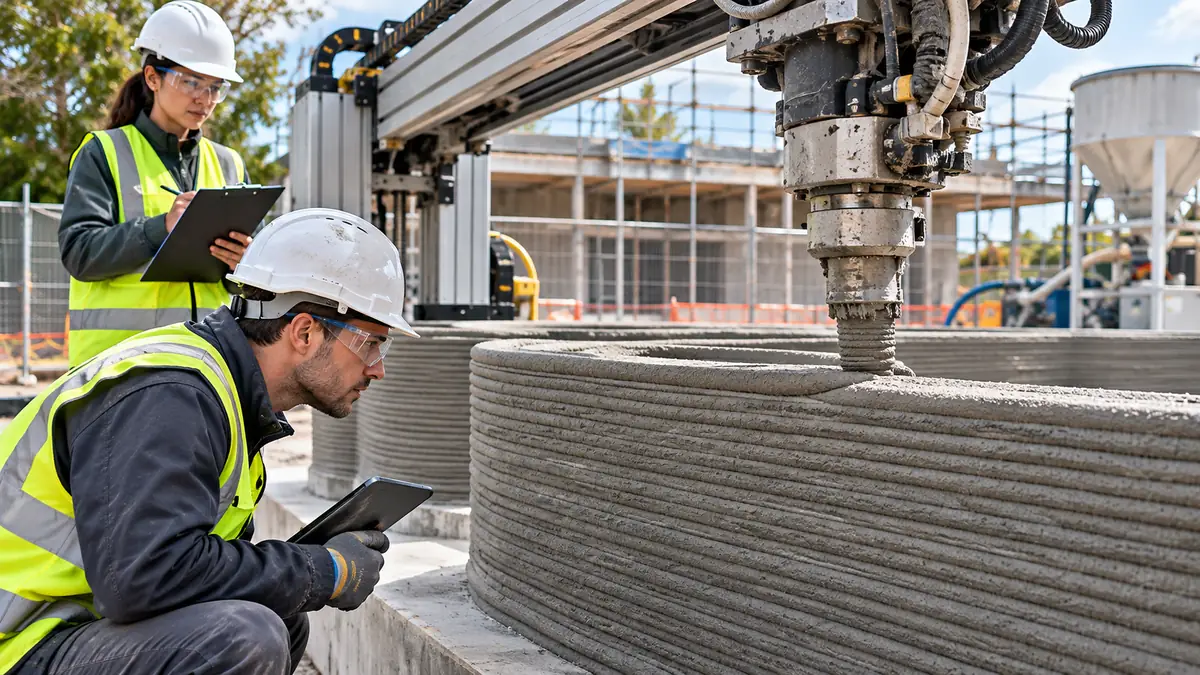
QA inspectors check the layers of a 3D concrete wall as a robotic printer deposits fresh concrete. image
3
3D Concrete Printing During-Print Quality Inspection Checklist
construction quality assurance +1

3D Concrete Printing During-Print Quality Inspection Checklist for one 3D concrete printing site visit, using approved project tolerances and documented inspection releases.
Review façade access and BMU requirements during design image
F
Review façade access and BMU requirements during design
construction safety +3

Review façade access and BMU interface requirements during design with an interactive checklist; commentable and export as PDF/Excel for safe façade access.
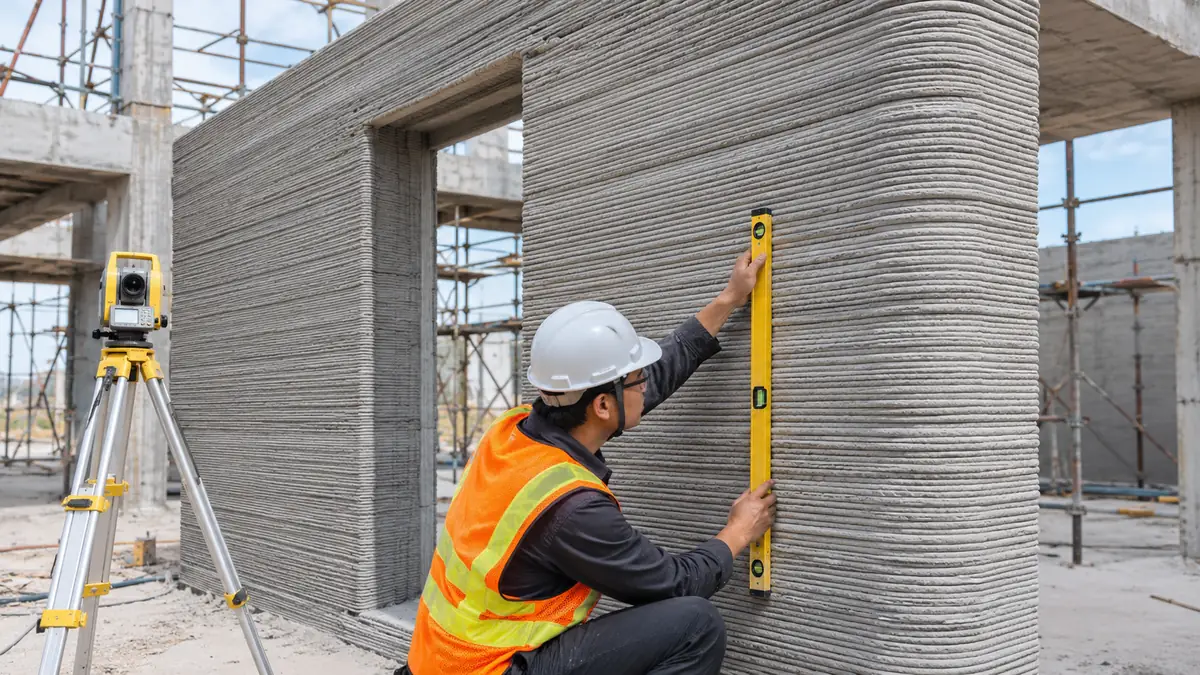
Engineer checks the plumbness and dimensions of a completed layered 3D printed concrete wall. image
3
3D Printed Concrete Completed Wall Inspection Checklist
construction quality assurance +1

3D Printed Concrete Completed Wall Inspection Checklist for one 3D concrete printing site visit, using approved project tolerances and documented inspection releases.
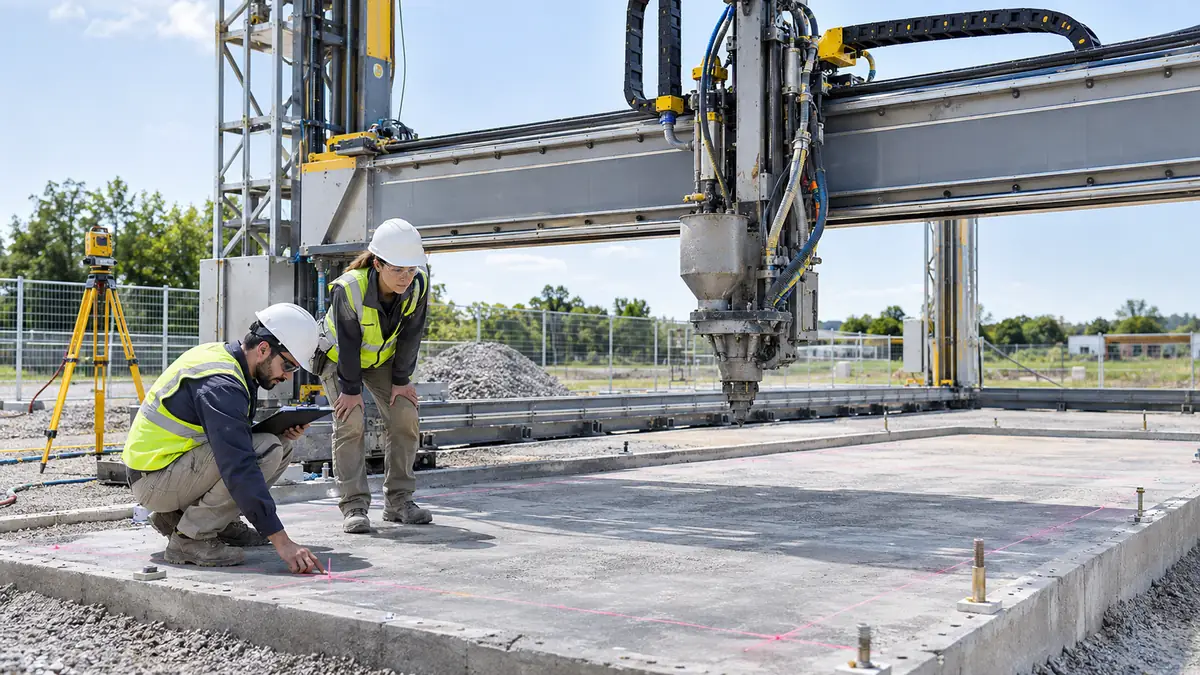
Site engineers verify foundation setting-out and printer readiness before 3D concrete wall printing starts. image
3
3D Concrete Printing Pre-Print Readiness Inspection Checklist
construction quality assurance +1

Pre-print 3D concrete printing inspection checklist for a single site visit: approved print files, foundation, printer calibration, materials, safety and release.
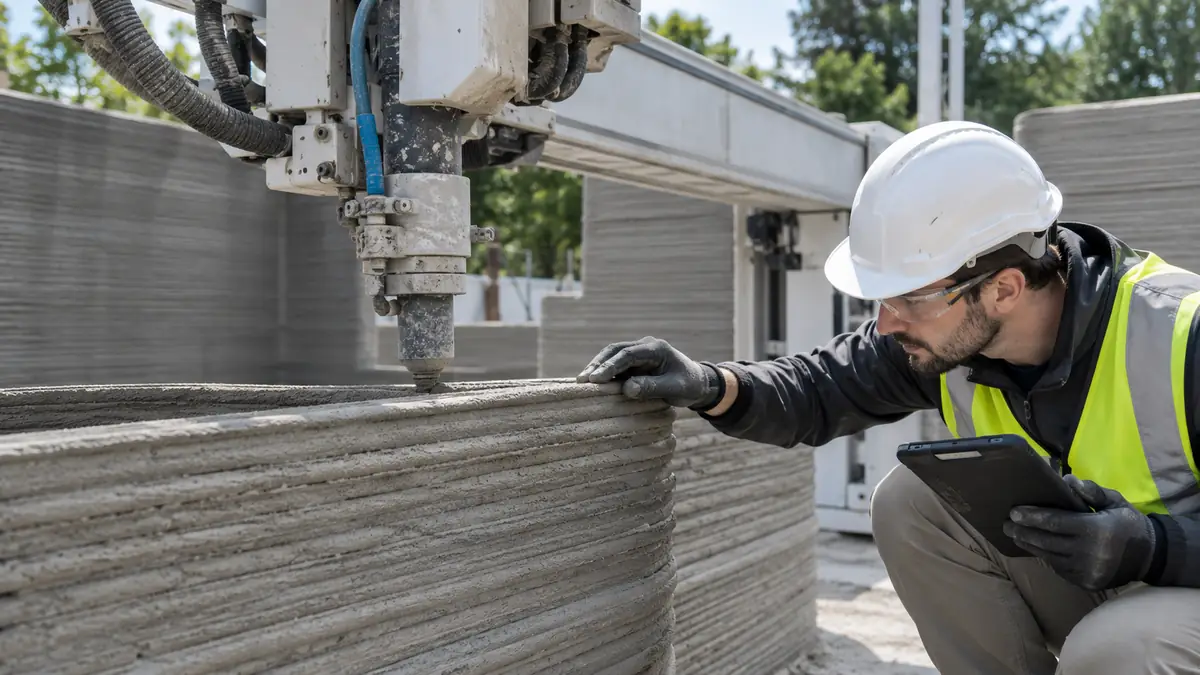
Site engineer inspects the last printed layer and nozzle position before restarting paused concrete 3D printing. image
3
3D Concrete Printing Interruption and Restart Inspection Checklist
construction quality assurance +1

3D Concrete Printing Interruption and Restart Inspection Checklist for one 3D concrete printing site visit, using approved project tolerances and documented inspection releases.
Review façade shading device design: projection & drainage image
F
Review façade shading device design: projection & drainage
construction quality assurance +3

Review façade shading device design for projection, drainage, and cleaning access with an interactive checklist—commentable—and export as PDF/Excel for approvals.