Inspect couplers and lap splices for piles with this field-ready checklist for QA/QC teams, verifying approvals, engagement lengths, torque, and witness marks while deliberately excluding cage fabrication tasks.
- Confirm approvals, models, and locations before any splicing proceeds.
- Measure engagement and lap lengths with traceable, photographed evidence.
- Apply specified torque with calibrated tools and witness marks.
- Interactive, commentable checklist; export reports with QR code verification.
The checklist
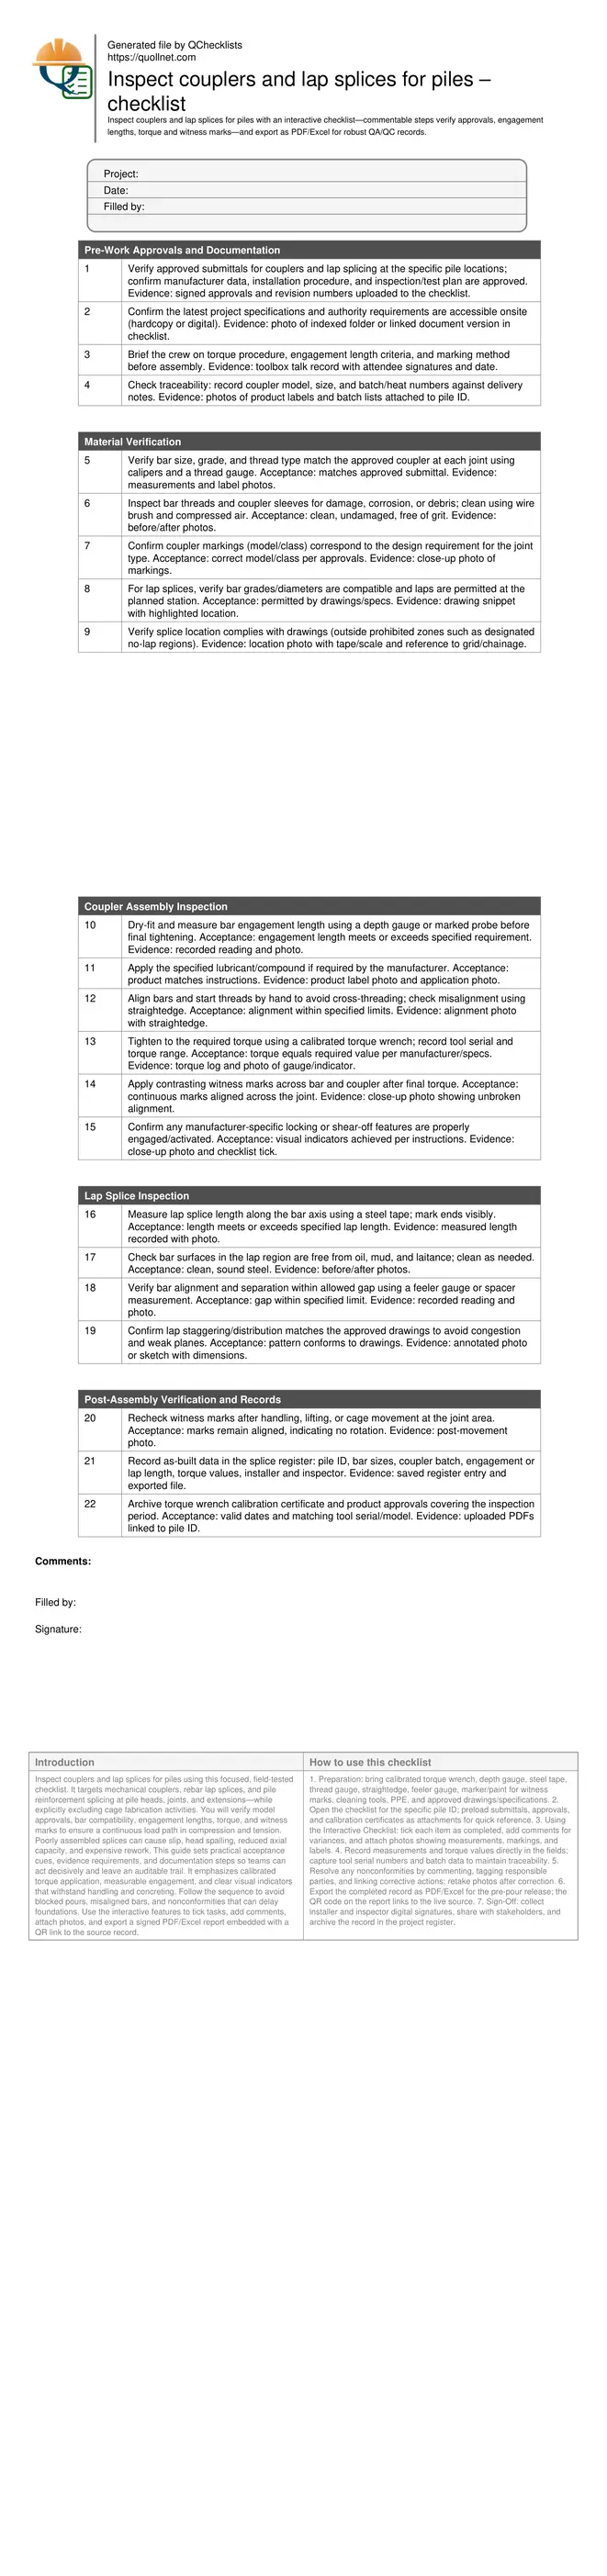
Pre-Work Approvals and Documentation
- Verify approved submittals for couplers and lap splicing at the specific pile locations; confirm manufacturer data, installation procedure, and inspection/test plan are approved. Evidence: signed approvals and revision numbers uploaded to the checklist.
- Confirm the latest project specifications and authority requirements are accessible onsite (hardcopy or digital). Evidence: photo of indexed folder or linked document version in checklist.
- Brief the crew on torque procedure, engagement length criteria, and marking method before assembly. Evidence: toolbox talk record with attendee signatures and date.
- Check traceability: record coupler model, size, and batch/heat numbers against delivery notes. Evidence: photos of product labels and batch lists attached to pile ID.
Material Verification
- Verify bar size, grade, and thread type match the approved coupler at each joint using calipers and a thread gauge. Acceptance: matches approved submittal. Evidence: measurements and label photos.
- Inspect bar threads and coupler sleeves for damage, corrosion, or debris; clean using wire brush and compressed air. Acceptance: clean, undamaged, free of grit. Evidence: before/after photos.
- Confirm coupler markings (model/class) correspond to the design requirement for the joint type. Acceptance: correct model/class per approvals. Evidence: close-up photo of markings.
- For lap splices, verify bar grades/diameters are compatible and laps are permitted at the planned station. Acceptance: permitted by drawings/specs. Evidence: drawing snippet with highlighted location.
- Verify splice location complies with drawings (outside prohibited zones such as designated no-lap regions). Evidence: location photo with tape/scale and reference to grid/chainage.
Coupler Assembly Inspection
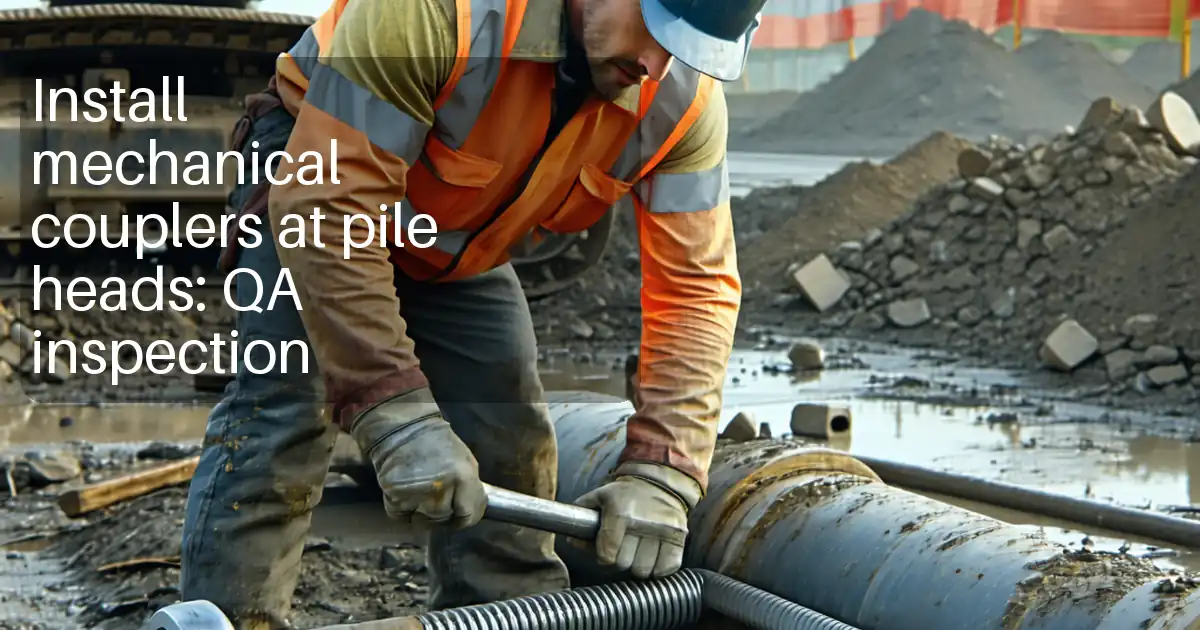
- Dry-fit and measure bar engagement length using a depth gauge or marked probe before final tightening. Acceptance: engagement length meets or exceeds specified requirement. Evidence: recorded reading and photo.
- Apply the specified lubricant/compound if required by the manufacturer. Acceptance: product matches instructions. Evidence: product label photo and application photo.
- Align bars and start threads by hand to avoid cross-threading; check misalignment using straightedge. Acceptance: alignment within specified limits. Evidence: alignment photo with straightedge.
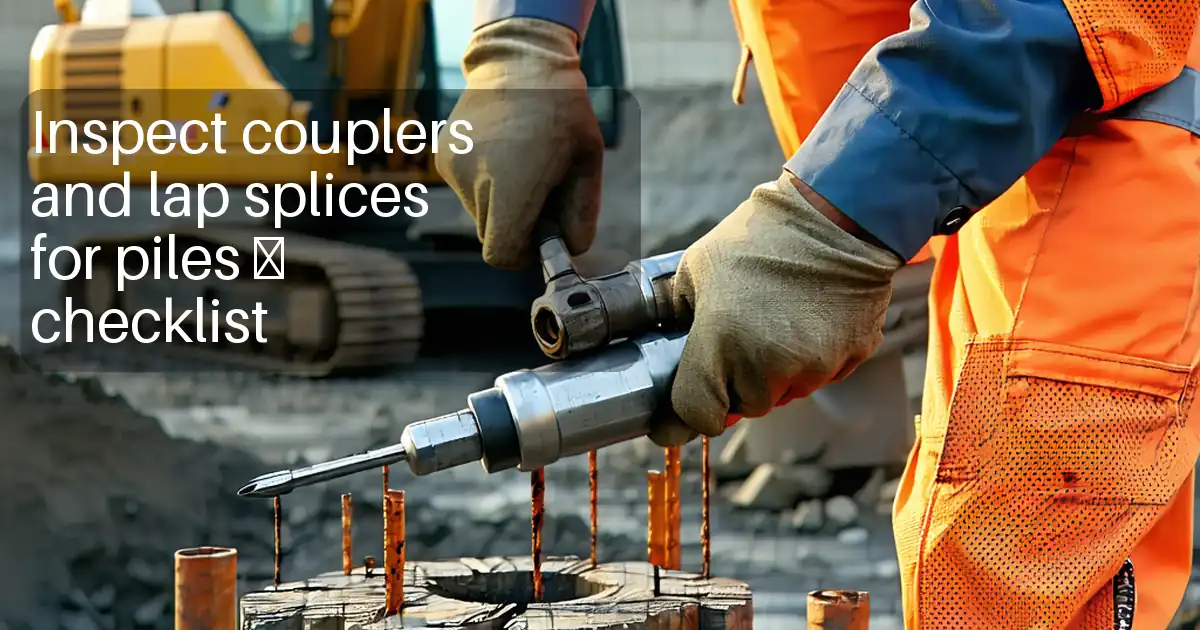
- Tighten to the required torque using a calibrated torque wrench; record tool serial and torque range. Acceptance: torque equals required value per manufacturer/specs. Evidence: torque log and photo of gauge/indicator.
- Apply contrasting witness marks across bar and coupler after final torque. Acceptance: continuous marks aligned across the joint. Evidence: close-up photo showing unbroken alignment.
- Confirm any manufacturer-specific locking or shear-off features are properly engaged/activated. Acceptance: visual indicators achieved per instructions. Evidence: close-up photo and checklist tick.
Lap Splice Inspection
- Measure lap splice length along the bar axis using a steel tape; mark ends visibly. Acceptance: length meets or exceeds specified lap length. Evidence: measured length recorded with photo.
- Check bar surfaces in the lap region are free from oil, mud, and laitance; clean as needed. Acceptance: clean, sound steel. Evidence: before/after photos.
- Verify bar alignment and separation within allowed gap using a feeler gauge or spacer measurement. Acceptance: gap within specified limit. Evidence: recorded reading and photo.
- Confirm lap staggering/distribution matches the approved drawings to avoid congestion and weak planes. Acceptance: pattern conforms to drawings. Evidence: annotated photo or sketch with dimensions.
Post-Assembly Verification and Records
- Recheck witness marks after handling, lifting, or cage movement at the joint area. Acceptance: marks remain aligned, indicating no rotation. Evidence: post-movement photo.
- Record as-built data in the splice register: pile ID, bar sizes, coupler batch, engagement or lap length, torque values, installer and inspector. Evidence: saved register entry and exported file.
- Archive torque wrench calibration certificate and product approvals covering the inspection period. Acceptance: valid dates and matching tool serial/model. Evidence: uploaded PDFs linked to pile ID.
Preview the printable checklist
Preview page one below. Open the image or download the PDF for all pages.
At a glance
- Purpose-built for pile splicing inspections, this checklist standardizes verification of approvals, bar compatibility, coupler model, engagement length, torque, and witness marks. It reduces ambiguity, speeds acceptance, and captures photos, measurements, and signatures that withstand audits and pre-pour hold points.
- Controls are optimized for deep foundation realities: limited access, congested steel, and tight pour timelines. Field methods rely on simple, durable tools—steel tape, depth gauge, torque wrench—to validate engagement and torque without disrupting reinforcement or concreting operations.
- Interactive online checklist with tick, comment, and export features secured by QR code.
- Outcomes include traceable torque logs, engagement measurements, and splice registers linked to pile IDs. The process prevents slippage, mislocation of laps, and unapproved couplers, helping avoid remedial works, claims, and schedule risk per approved project specifications and authority requirements.
How to use this interactive pile splice inspection checklist
- Preparation: bring calibrated torque wrench, depth gauge, steel tape, thread gauge, straightedge, feeler gauge, marker/paint for witness marks, cleaning tools, PPE, and approved drawings/specifications.
- Open the checklist for the specific pile ID; preload submittals, approvals, and calibration certificates as attachments for quick reference.
- Using the Interactive Checklist: tick each item as completed, add comments for variances, and attach photos showing measurements, markings, and labels.
- Record measurements and torque values directly in the fields; capture tool serial numbers and batch data to maintain traceability.
- Resolve any nonconformities by commenting, tagging responsible parties, and linking corrective actions; retake photos after correction.
- Export the completed record as PDF/Excel for the pre-pour release; the QR code on the report links to the live source.
- Sign-Off: collect installer and inspector digital signatures, share with stakeholders, and archive the record in the project register.
Why coupler and lap splice inspections matter in piles
In deep foundations, splices must transmit axial, shear, and bending demands without slip. Mechanical couplers and rebar lap splices in piles are often installed under time pressure around cutoff levels or segment joints. Focused inspection prevents hidden defects—cross-threading, insufficient engagement length, under-torque, or misplaced laps—that can reduce capacity and cause head spalling or settlement. A simple sequence works: confirm approvals, verify materials, measure engagement or lap length, apply calibrated torque, and mark the joint so any movement is obvious. Photographic evidence with scales, torque logs, and batch records build an auditable trail for pre-pour releases. This checklist keeps scope tight around couplers and lap splices only; cage fabrication tasks are purposely excluded. When followed, it reduces rework, shortens hold points, and improves confidence during concreting, especially where access is restricted and visibility is limited.
- Verify approvals, then inspect materials before assembly.
- Measure engagement or lap length and record readings.
- Apply specified torque using a calibrated wrench.
- Use witness marks to detect post-assembly movement.
Field methods to verify engagement lengths and torque
Engagement length is the backbone of a coupler’s performance. Mark bar insertion using a depth gauge or a tape and scribe line to confirm minimum engagement before torqueing. During tightening, use a calibrated torque wrench sized for the range; take steady, smooth pulls and avoid dynamic impacts that inflate readings. Note wrench serial numbers, calibration validity, and target torque in a log, then photograph the gauge or digital screen at peak. After final tightening, paint contrasting witness marks across the coupler and bar. If anything shifts during lifting or positioning, misalignment becomes obvious. These steps are fast but powerful, providing a measurable check on load transfer. Always store evidence in the splice record tied to the pile ID so inspectors and clients can verify performance later per approved project specifications and authority requirements.
- Measure insertion depth before final torque.
- Tighten with a calibrated torque wrench only.
- Log torque values, tool serials, and dates.
- Apply and photograph contrasting witness marks.
Lap splice controls inside piles without touching cage fabrication
Lap splices rely on sufficient length, correct location, and adequate contact. Start by confirming that laps are permitted at the station and that bar grades and diameters match drawings. Measure lap length along the bar axis with a steel tape and clearly mark lap ends for visibility. Check alignment and separation with a feeler gauge to ensure the gap is within allowed limits; clean the steel to remove mud or oil that can impair bond. Avoid shifting reinforcement or making fabrication changes—this checklist solely inspects the splice itself. Document the lap position relative to grid/chainage and confirm any required staggering pattern from drawings. Photos with scales and a short sketch make acceptance straightforward during pre-pour inspections.
- Confirm laps are permitted at the planned location.
- Measure lap length and mark ends visibly.
- Keep bars clean and gaps within limits.
- Record position and staggering with photos/sketch.